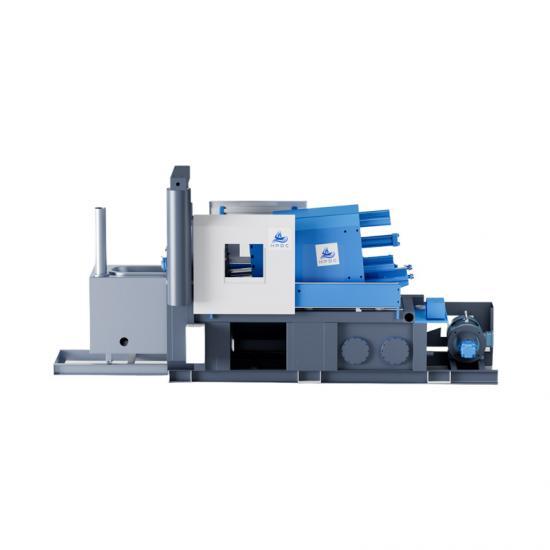
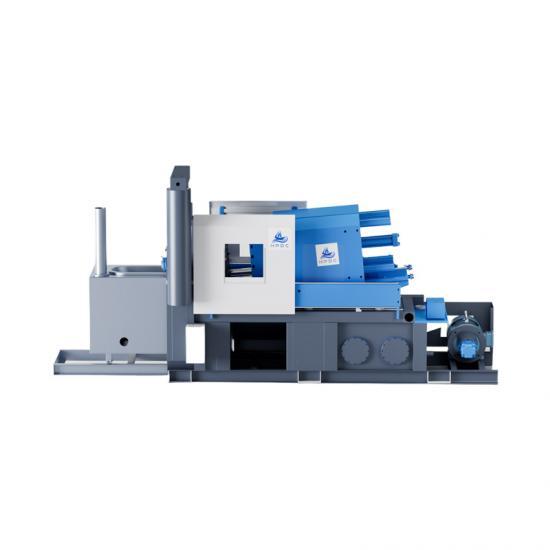
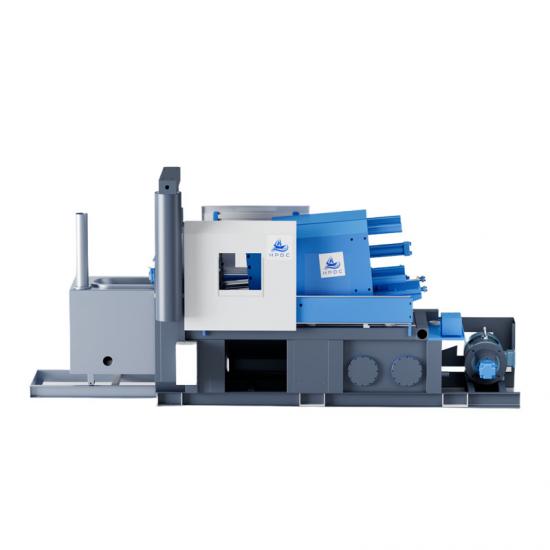
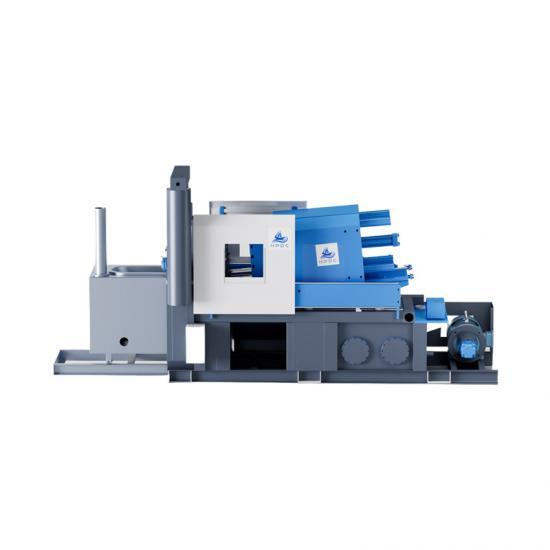
Core Selling Point
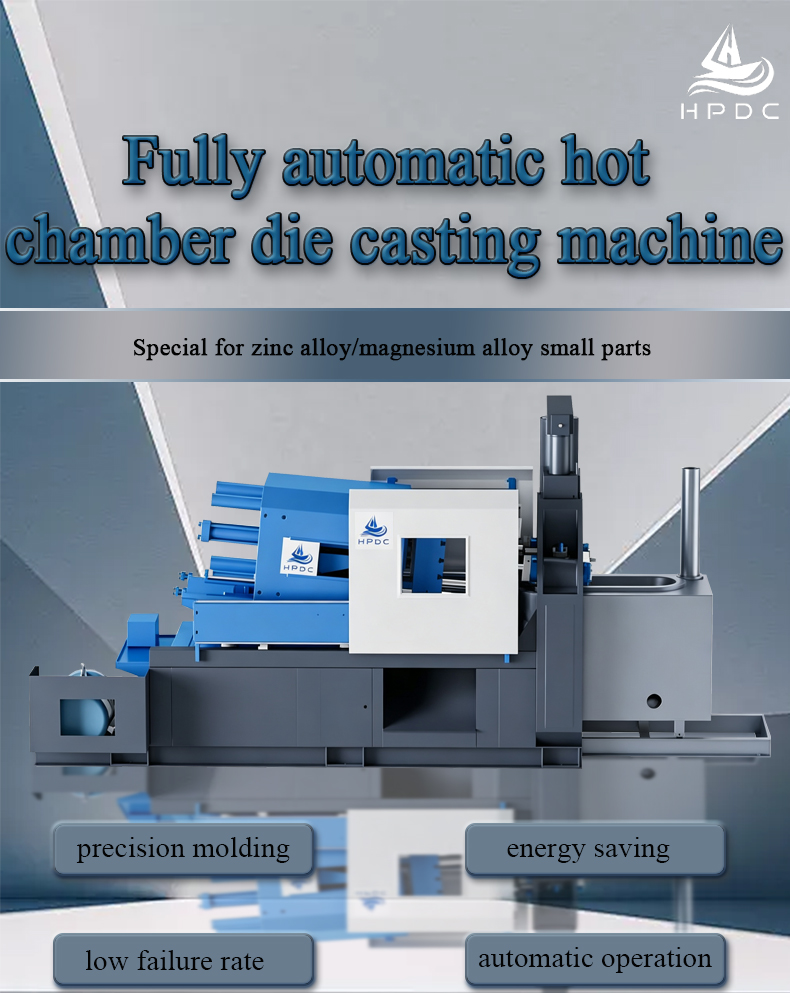
✅Complete tonnage coverage, from small parts with multiple cavities to large parts, there are corresponding models
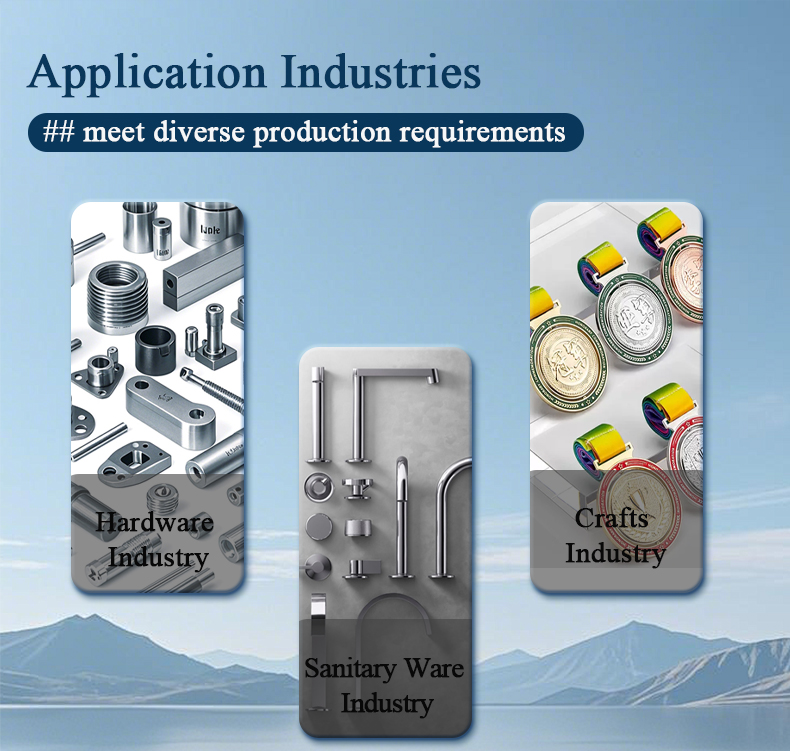
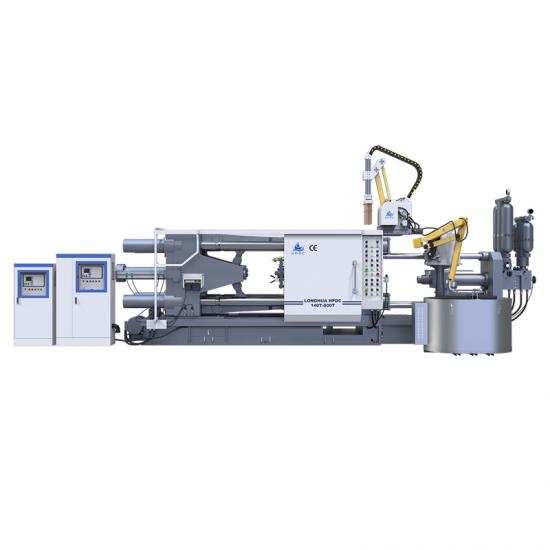
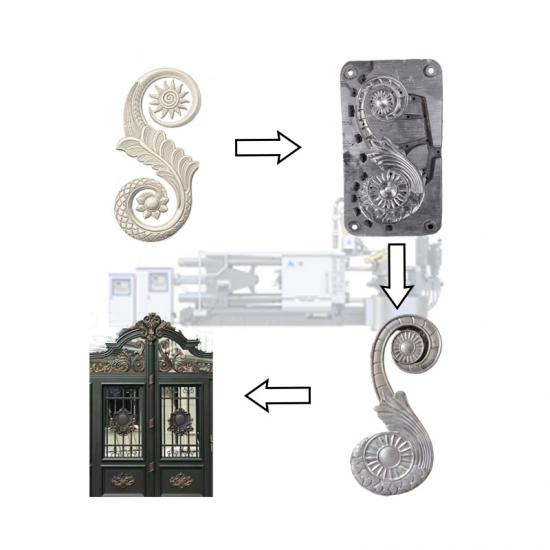
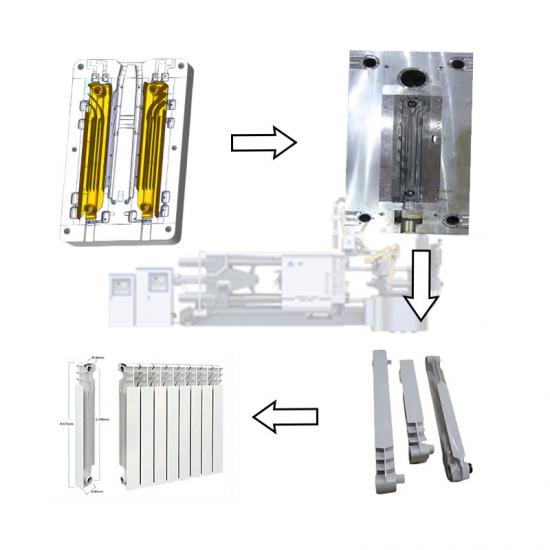
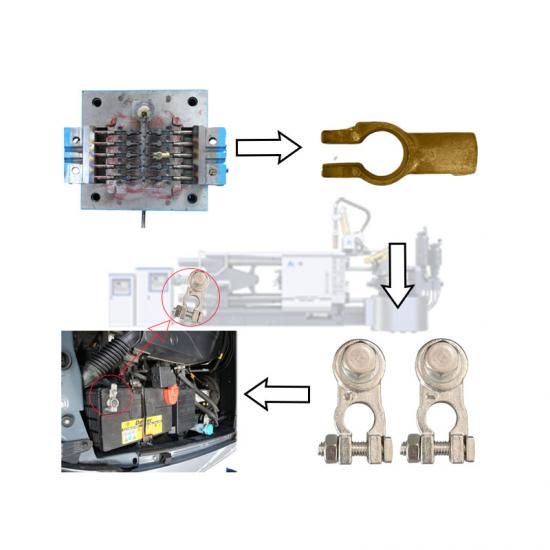
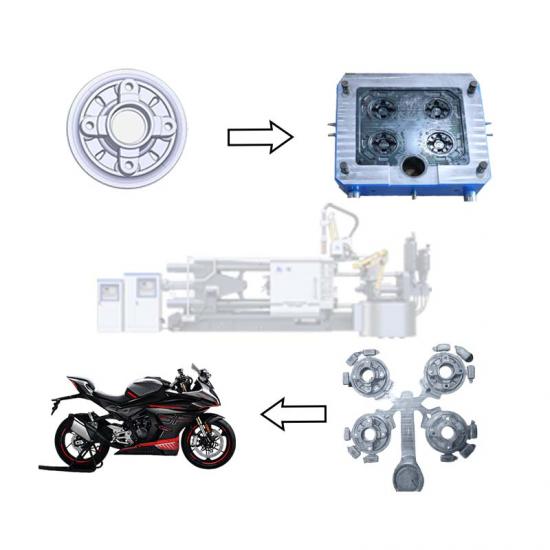
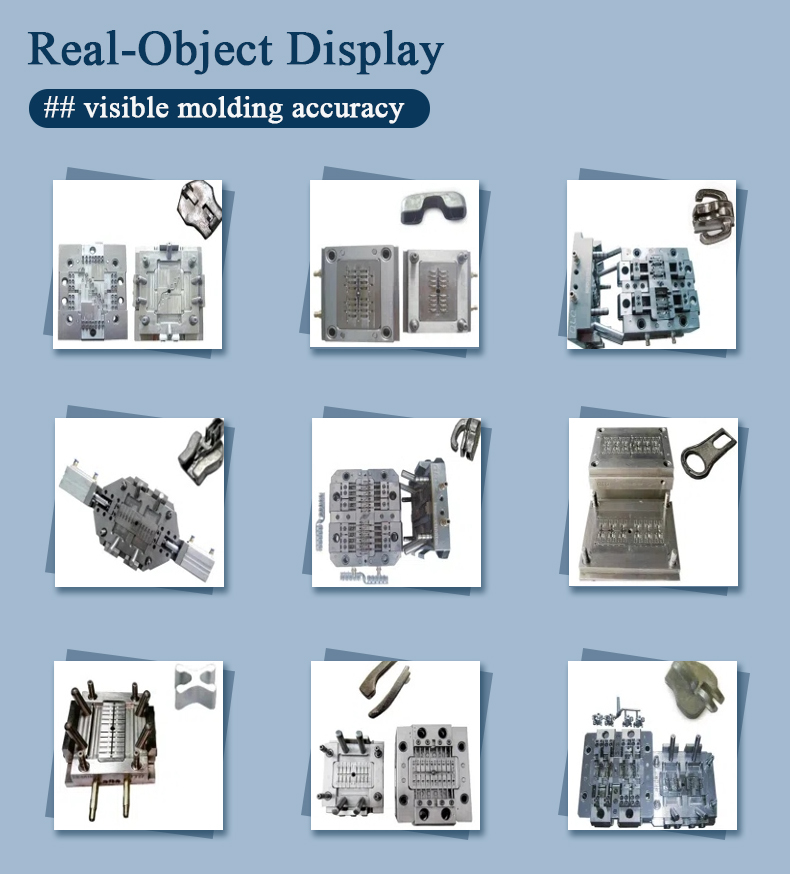
30T–450T complete sequence: small tonnage is suitable for multi-cavity small precision parts such as buttons and zipper pullers; medium and large tonnage can be used for large-sized zinc alloy parts such as locks, brackets, car models, etc. When customers expand production, they can be smoothly upgraded within the same brand series, and the processes and accessories are common.
✅The hot chamber supplies ingredients in one piece, eliminating the need for soup, fast pace and low loss
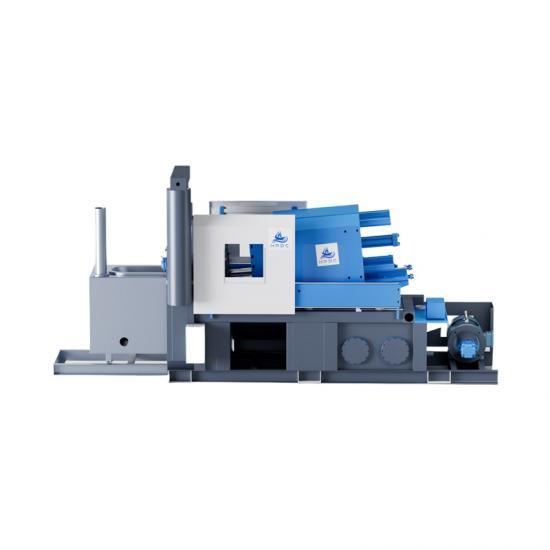
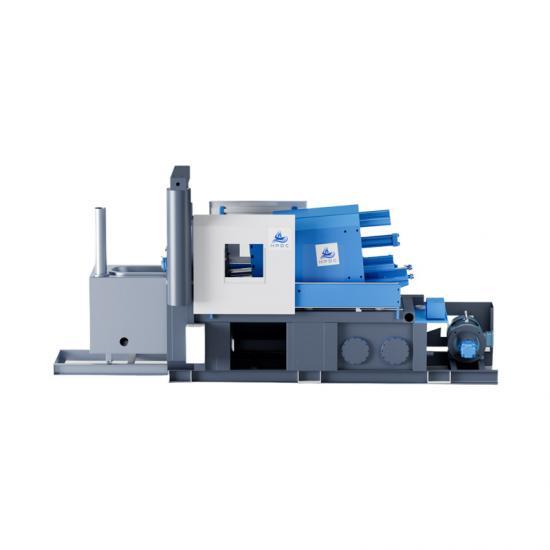
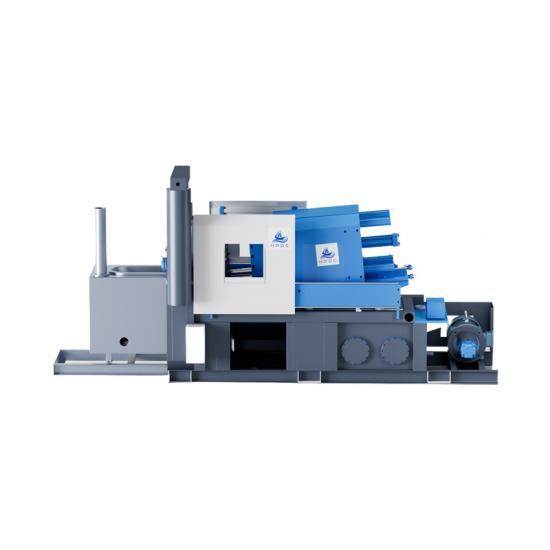
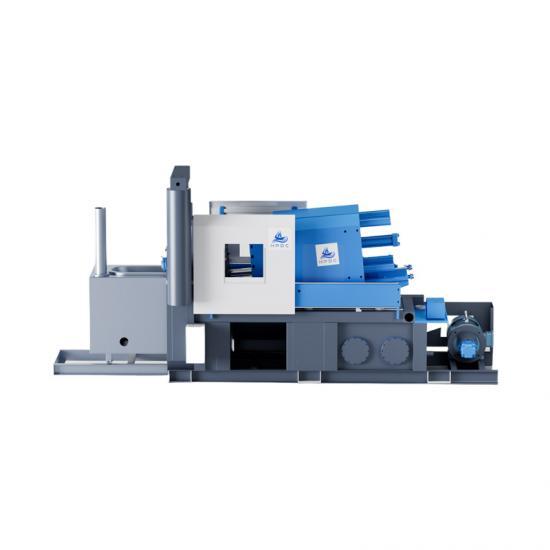
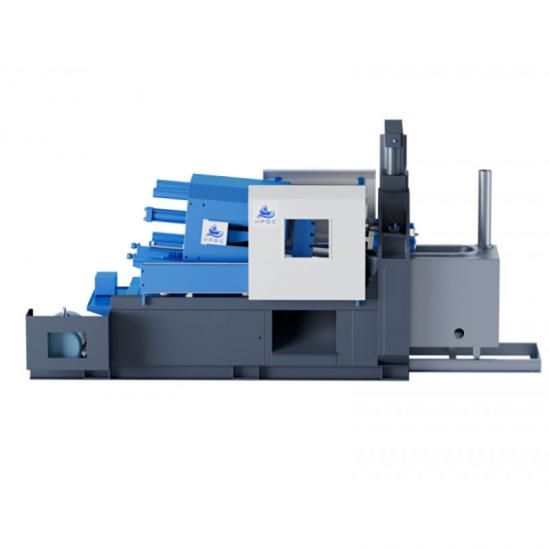
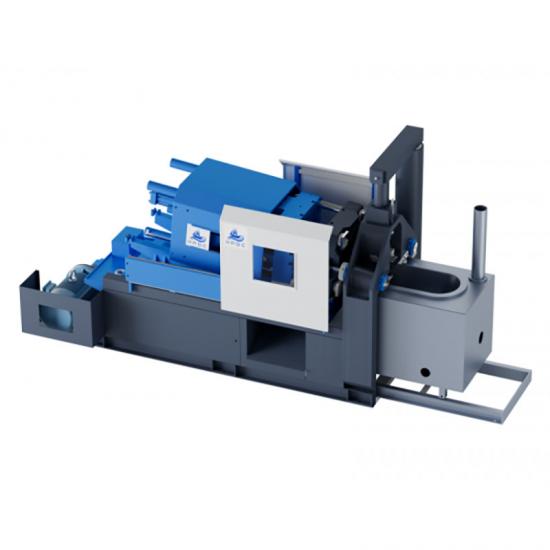
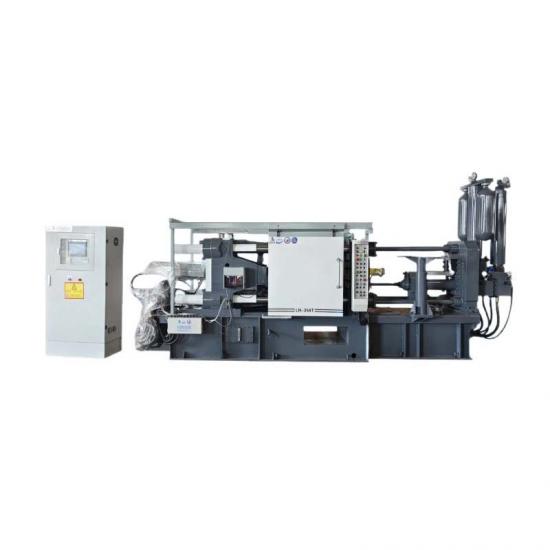
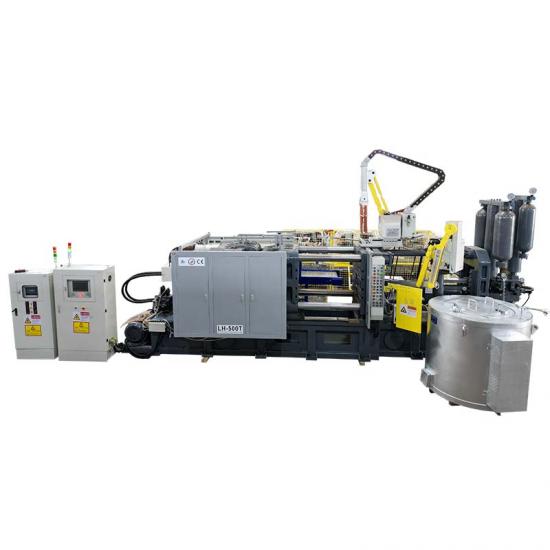
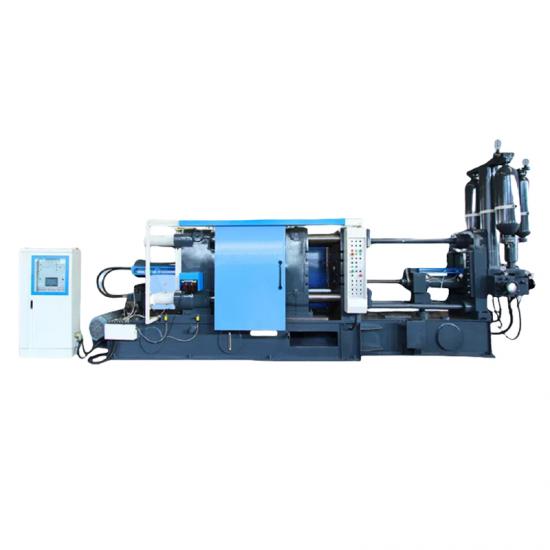
The crucible has a built-in machine, and the molten metal is directly pressed into the mold cavity through the gooseneck. There is no need to scoop the material separately for soup. The cycle time is short and the oxidation and burning loss is small. It is suitable for high-speed continuous production of small parts and the daily output of a single machine is high.
✅PLC segmented injection + optional servo, accurate molding, energy saving and material saving
The computer PLC adjusts the injection speed, pressurization, holding pressure and cooling time in stages, and multiple sets of mold recipes can be called with one click; the servo configuration supplies oil on demand, reducing no-load energy consumption. The surface of the casting is smooth, with few pores and flash, and the molding consistency is good.
✅The clamping rigidity is sufficient to protect the mold and reduce flash
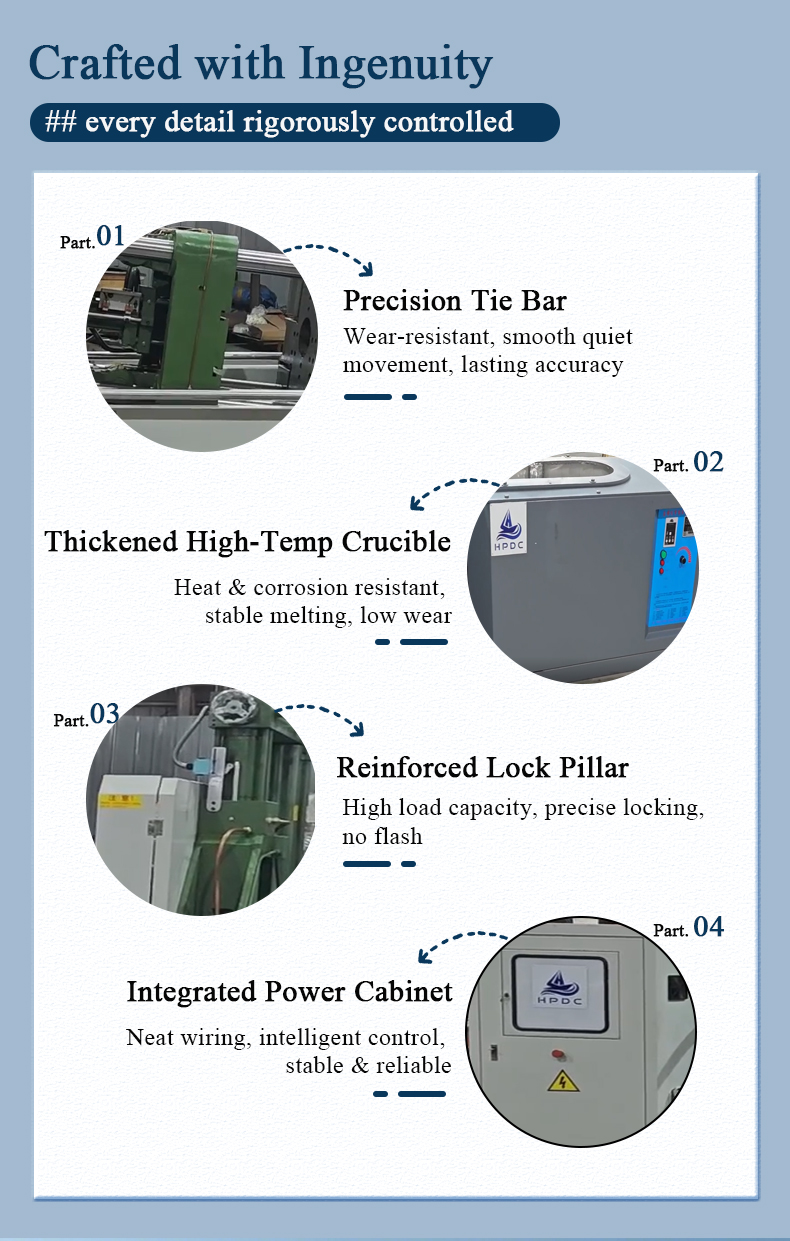
The fuselage is made of carbon steel welded, and key parts are heat treated to strengthen it. The inner distance of the coring pillar and the mold opening stroke are matched according to the tonnage. The mold clamping is stable and the impact is small. Complex parts and deep cavity parts are not easy to run out of materials and flash, and the mold life is guaranteed.
✅Strong automation expansion capability, can form a fully automatic die-casting island
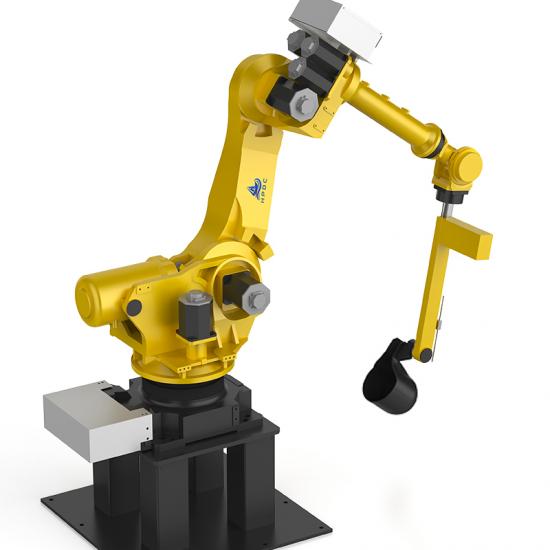
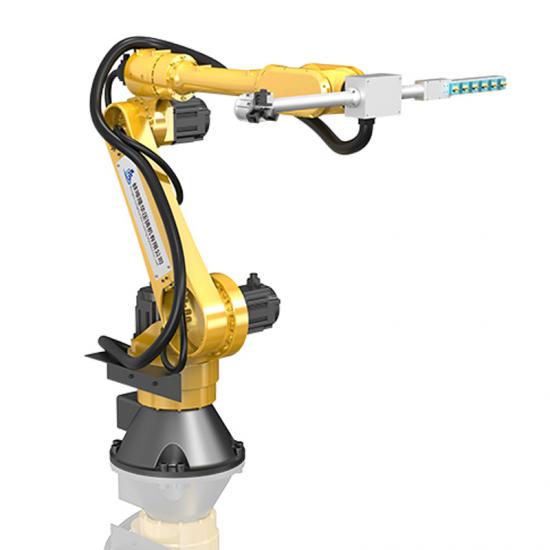
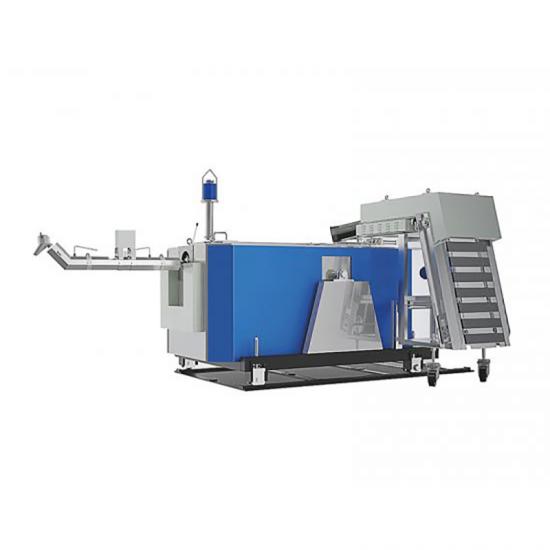
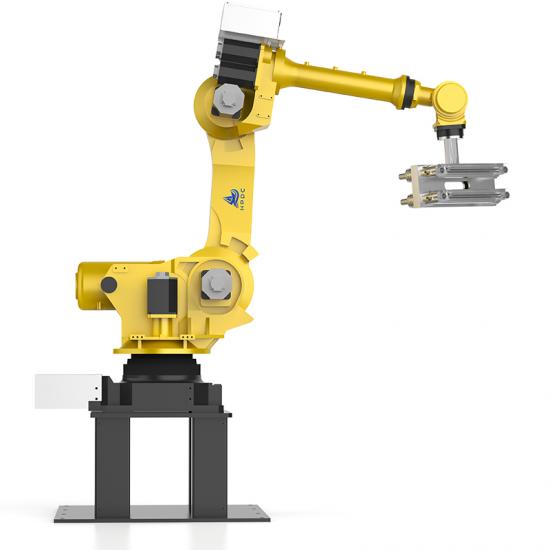
Interfaces for spraying, picking up, and conveyor belts are reserved, and can be used with Longhua servo sprayers, picking manipulators, industrial robots, and conveyor belts for online production; the original complete machine + peripheral equipment + consumables are included, and debugging and after-sales are completed in one stop.
✅Common accessories and perfect after-sales system
The material pot, gooseneck, nozzle, injection head, injection rod, nozzle, heating sheath and other consumable parts are supplied from the original factory; we provide pre-production samples, final factory inspection, video troubleshooting, on-site guidance from engineers and a priority policy for upgrading old customers.
Working Cycle Of Hot Chamber Die Casting Machine
-
Mold clamping: The movable platen moves forward, the mold is closed and locked, and the nozzle tip presses against the mold gate.
-
Feeding (plunger upward): The plunger in the injection cylinder moves upward, opening the feed port, and the molten metal flows into the injection cylinder by gravity.
-
Injection (plunger downward): The plunger moves downward to seal the feed inlet, hydraulically pump the metal into the gooseneck, and inject it into the closed cavity through the nozzle at high speed.
-
Pressurization and pressure-maintaining: After the cavity is filled, it is pressurized and compacted, and the metal solidifies and shrinks under pressure.
-
Cooling and solidification: maintain pressure until the casting solidifies, and the nozzle tip maintains temperature to prevent metal from solidifying in the flow channel.
-
Mold opening and ejection: After the mold is opened and the casting is ejected, the plunger returns to the upper position and enters the next cycle.
Product Parameters
Item
|
Unit
|
LH-HC-58T
|
Die-locking Force
|
kN
|
580
|
Die-stroke
|
mm
|
210
|
Clearance Between Tie Bars
|
mm
|
311*311
|
Die Thickness(Min/Max)
|
mm
|
120/320
|
Ejection Force
|
kN
|
50
|
Ejection Stroke
|
mm
|
60
|
Injection Force
|
kN
|
60
|
Plunger Stroke
|
mm
|
130
|
Shot Position
|
mm
|
0,-50
|
Plunger-tip Diameter
|
mm
|
45,50
|
Shot Weight(Zn)
|
kg
|
1.3
|
Working pressure
|
MPa
|
11.5
|
Motor Rating
|
kW
|
9.5
|
Melting Pot Capacity
|
kg
|
200
|
Oil Consumption Of Burner
|
kg/h
|
1.5~6.0
|
Oil Tank Capacity
|
L
|
310
|
Weight Of Machine
|
kg
|
3500
|
Size(L/W/H)
|
mm
|
3600x1500x2000
|
(Note: We reserve the right to make any technical improvements without prior notice)
Company Introduction
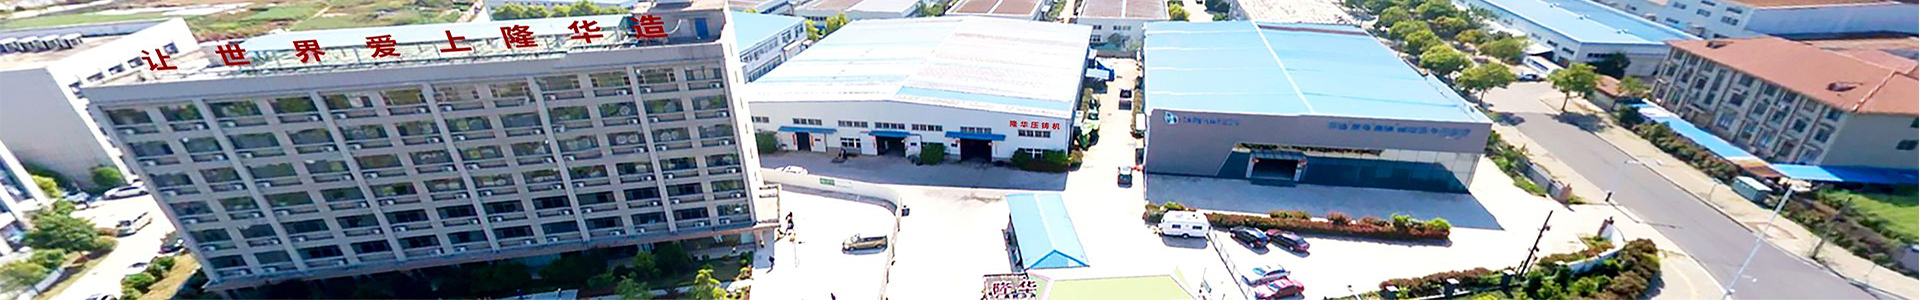
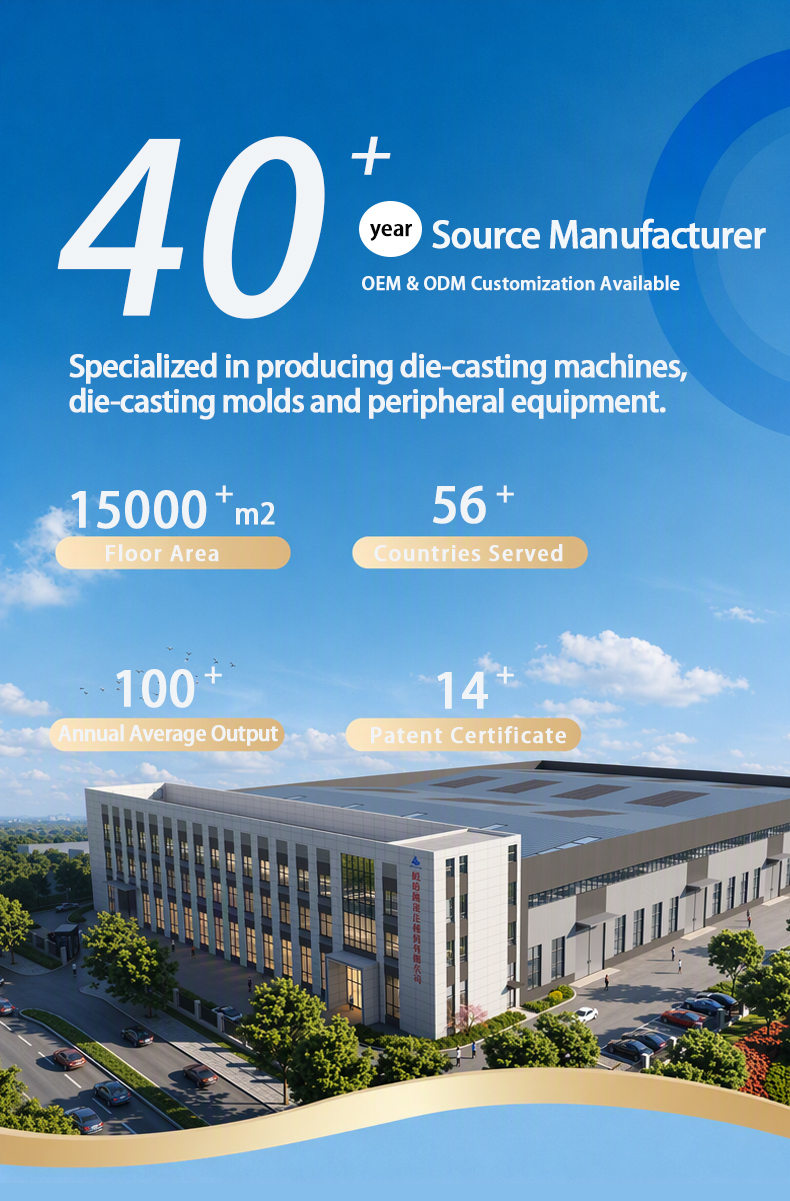
Bengbu Longhua Die casting Machine Co., Ltd. is based in Bengbu, Anhui — a time-honored industrial base and national comprehensive transportation hub. We are a high-tech enterprise specialized in the design, R&D, manufacturing, sales and global after-sales service of die-casting machines and supporting equipment.
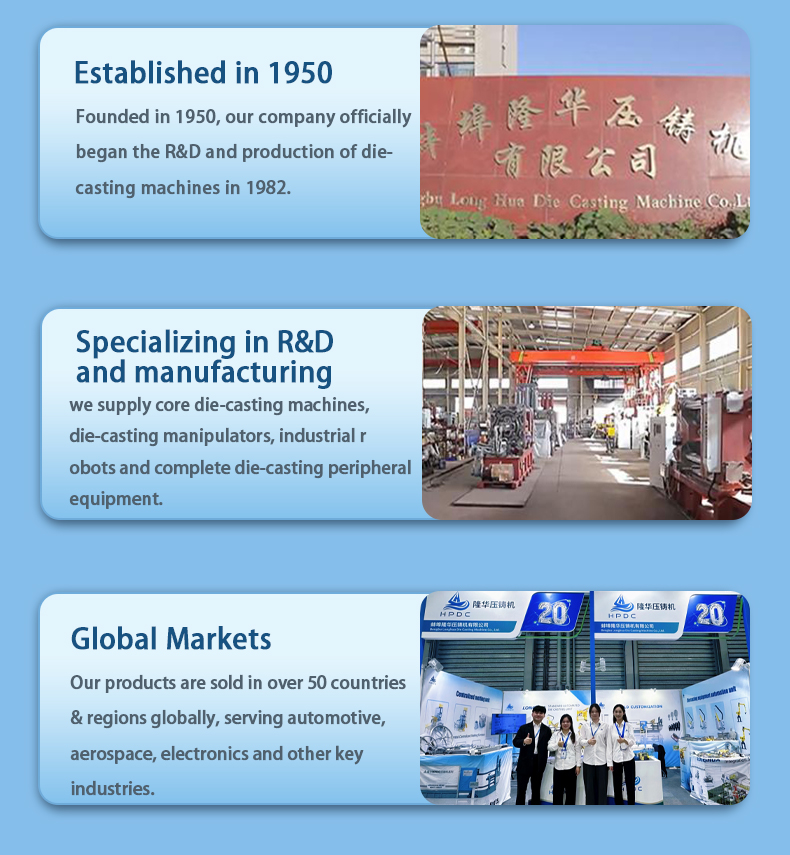
Dating back to 1950, Longhua officially began die-casting machine R&D and production in 1982. As a pioneer in China’s die-casting machinery sector, we have decades of industry expertise, continuous technical innovation and product upgrades.
Our full-range product portfolio covers cold chamber and hot chamber die-casting machines, together with die-casting manipulators, industrial robots and other auxiliary equipment. We deliver integrated die-casting production solutions for diverse industries.
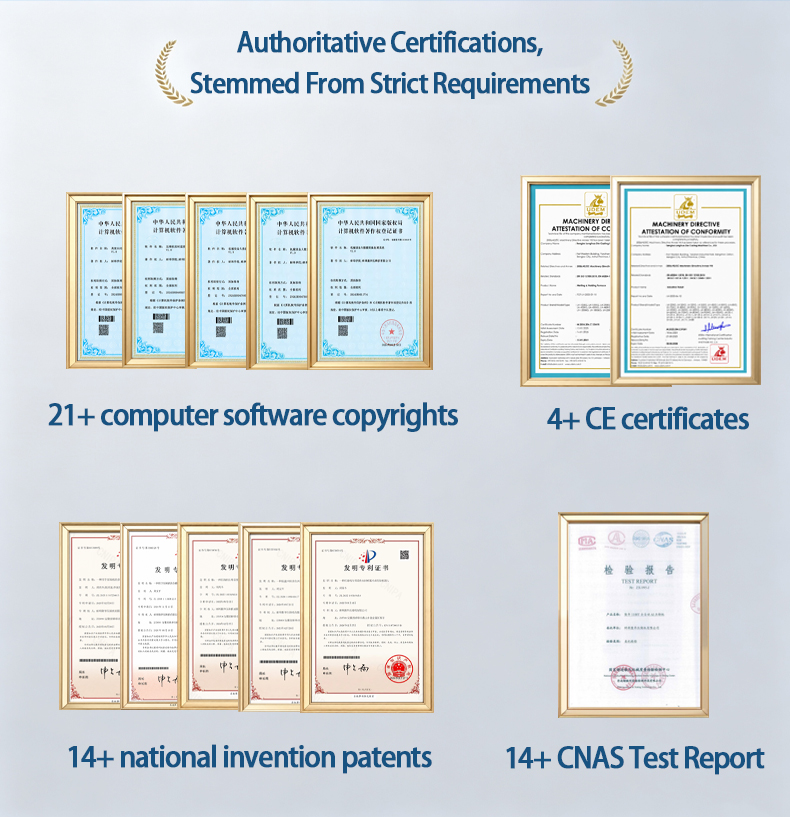
We boast strong innovation strength, holding over 14 invention patents and 21 software copyrights. We also lead the development of the group standard for Artificial Intelligence Cold Chamber Die Casting Machine. Our products are backed by CNAS test reports and CE certificates for reliable quality compliance.
Our equipment has been exported to over 50 countries and regions worldwide. Featuring stable performance and high production efficiency, our machines serve core sectors including automotive manufacturing, aerospace and electronic information, winning wide recognition from global customers.
FAQ
Q1: How long is the service life of a hot chamber gooseneck?
Under standard zinc alloy working condition, normal service life is 3,000–12,000 hours, depending on alloy purity, temperature control and daily maintenance.
Q2: What tonnage hot chamber machine should I choose? How to judge?
Priority is given to the projected area of the casting + whether it is a thin-walled and complex part. 30–90T is suitable for buttons, zipper pulls, small nameplates, and small multi-cavity parts; 130–200T is suitable for small and medium-sized parts such as locks, luggage buckles, handles, and instruments; 280–450T is suitable for brackets, car models, and larger casings. You provide casting drawings, product weight, and projected area, and we can help select models and calculate the clamping force for free.
Q3: What is the difference between hot chamber machine and cold chamber die casting machine? How should I choose?
The hot chamber comes with its own crucible and gooseneck for feeding materials, without the need for a soup feeding manipulator. It has a fast rhythm and less oxidation, and is suitable for large batches of small zinc alloy parts. The cold chamber requires separate melting and feeding, and is suitable for aluminum alloy, large parts, and thick-walled die-casting parts. Zinc alloys are given priority in hot chambers, while aluminum alloys must be placed in cold chambers.
Q4: Is hot chamber die casting suitable for high volume or low volume production?
It is most cost-effective for high-volume mass production. High mold cost makes it less economical for small batch or prototype orders.
Q5: What is the fastest machine cycle time?
The cycle time depends on the product size, wall thickness, cooling time, and mold structure. Small multi-cavity products can achieve a cycle of several seconds; medium and large parts have a long cooling time and the cycle time will be extended. A sample mold trial can be provided to confirm the stable cycle time.
Q6: What defects often occur in hot chamber zinc die casting?
Common defects: porosity, cold shut, flash, shrinkage sink, nozzle clogging, gooseneck erosion. Most can be optimized by process and machine adjustment.
Q7: Does the machine come with a furnace? Do I still need to buy a smelting furnace separately?
The LH-HC hot chamber die-casting machine has a built-in integrated crucible melting furnace, which does not require a separate external melting furnace. The metal is melted and kept warm directly in the crucible of the machine, eliminating the need for a soup process.
Q8: Is there CE certification? Can it be exported?
Supporting foreign trade exports, we can provide CE certificates, factory inspection reports, packing lists, invoices and other customs clearance information; nameplates and instructions in English can be made according to customer requirements.