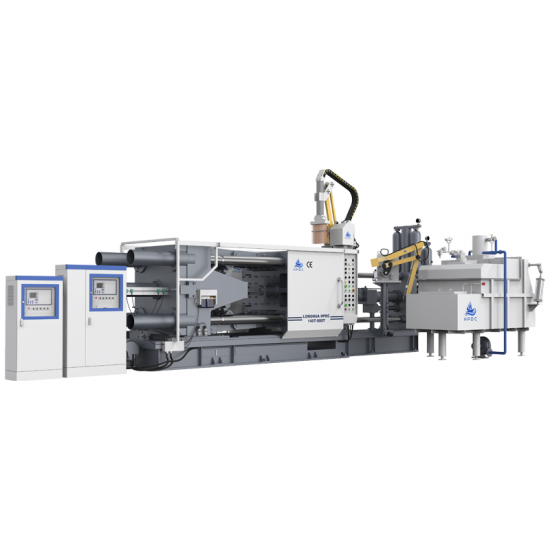
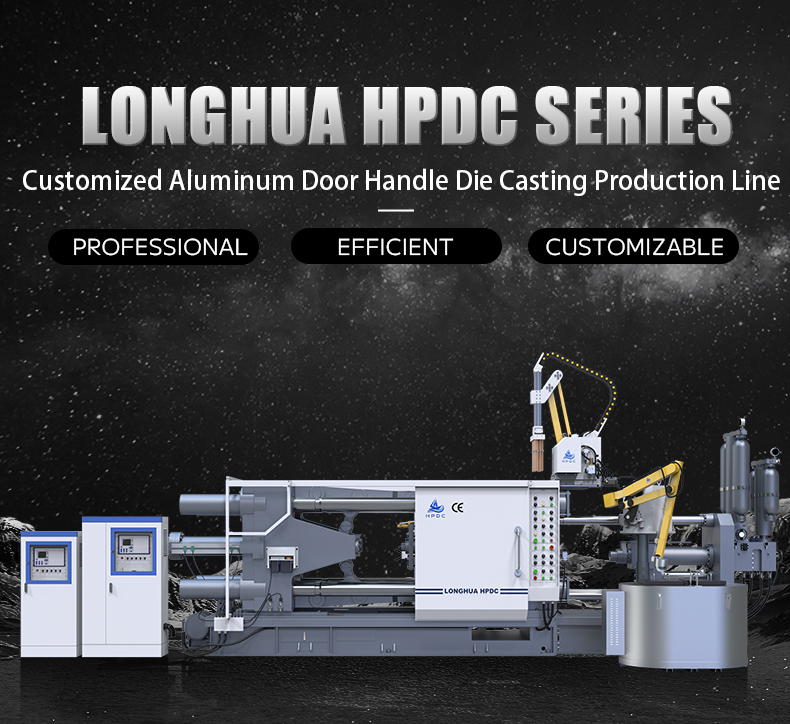
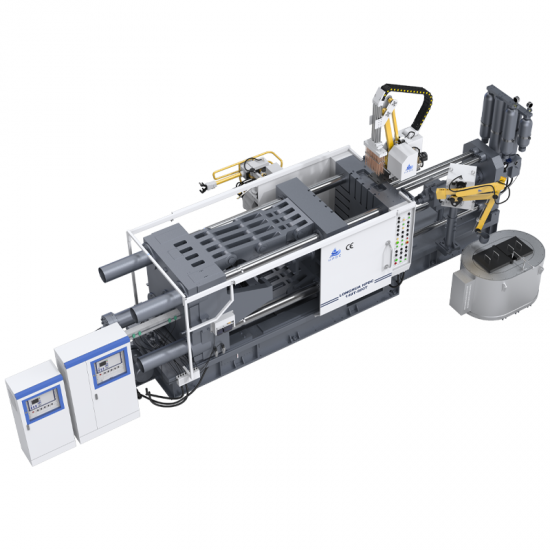
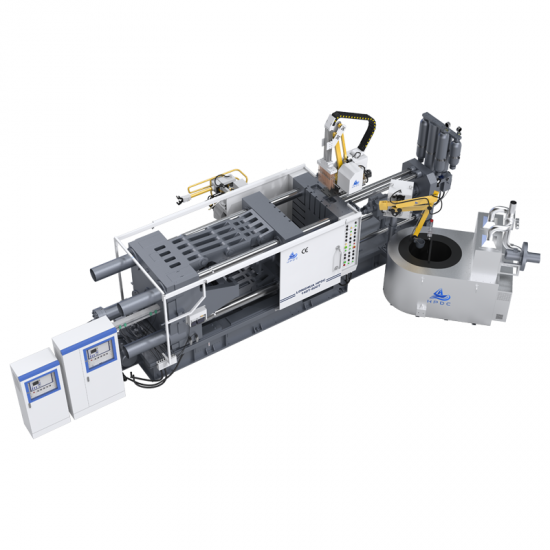
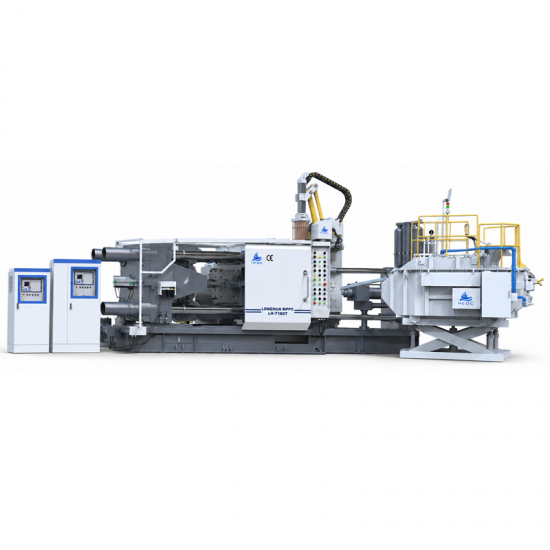
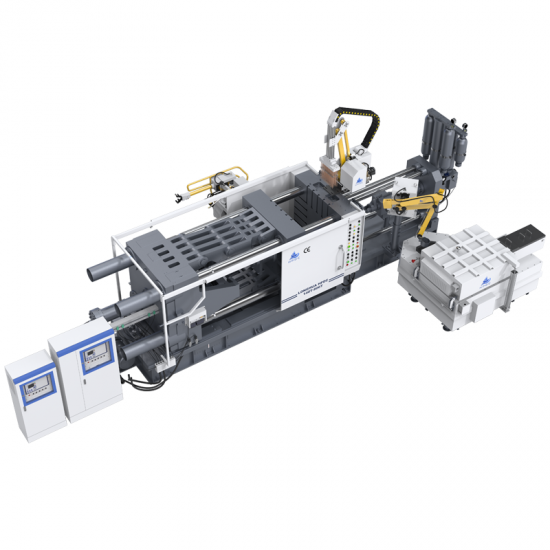
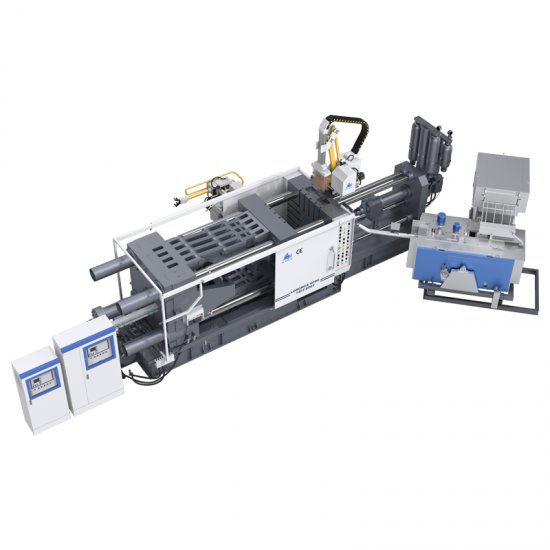
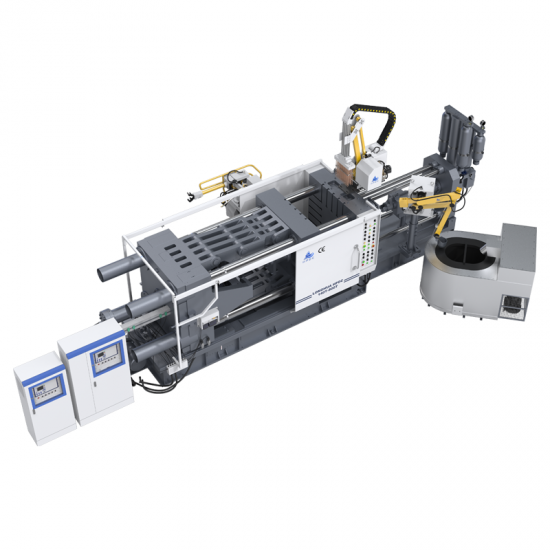
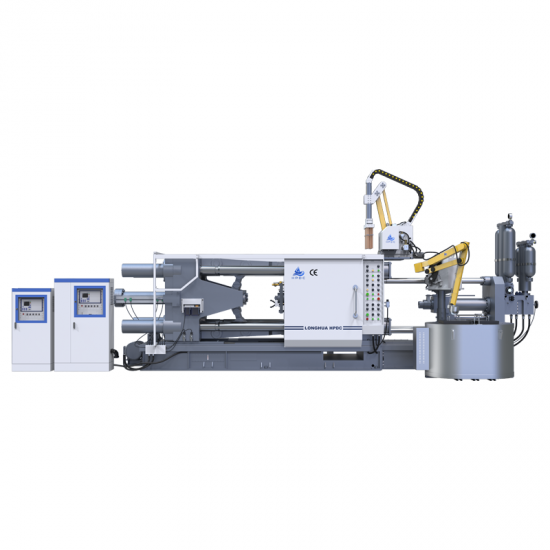
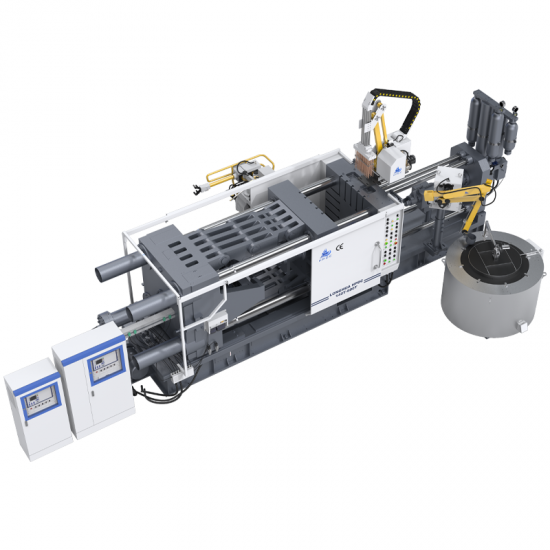
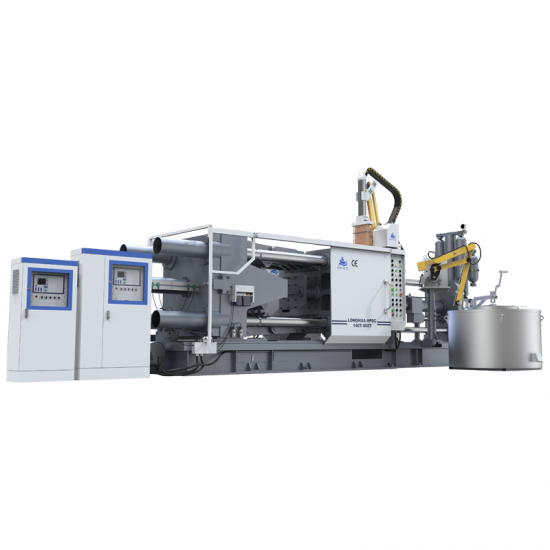
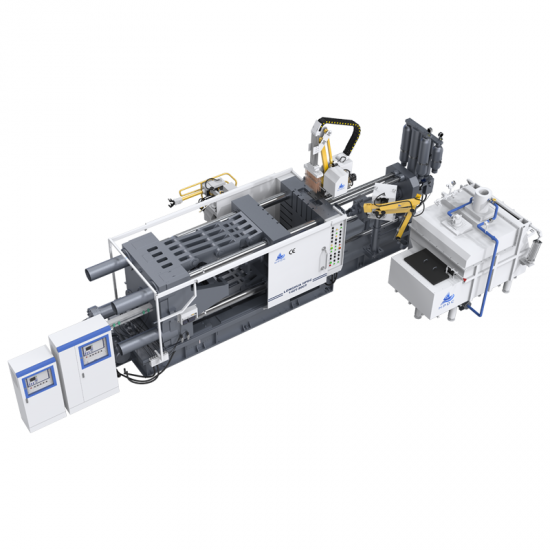
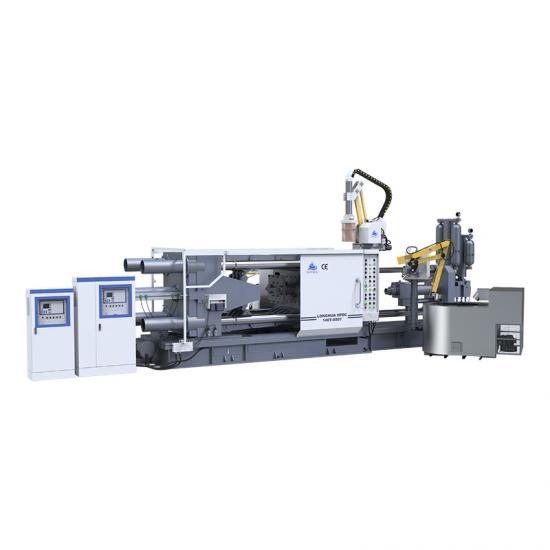
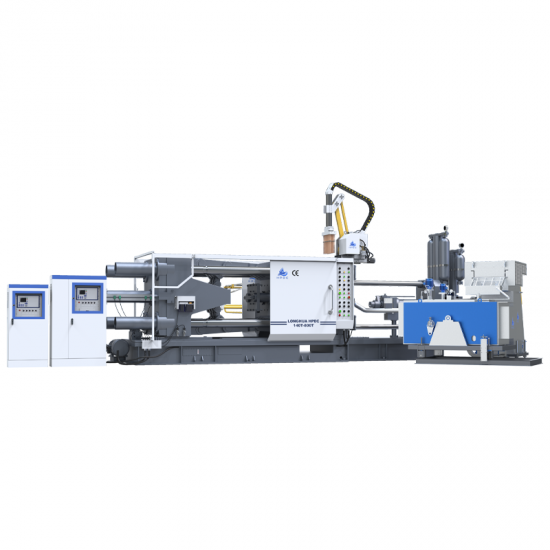
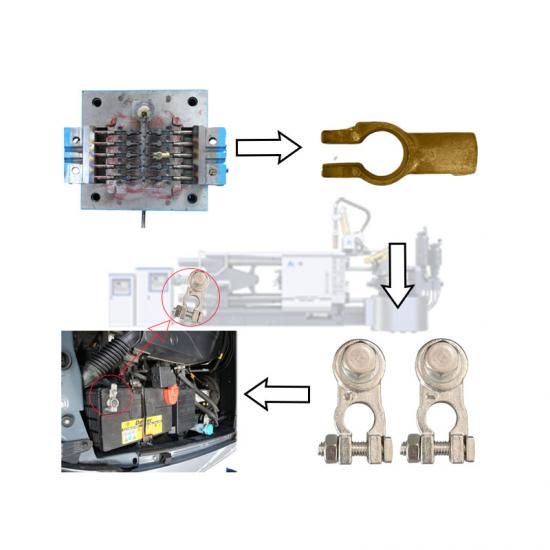
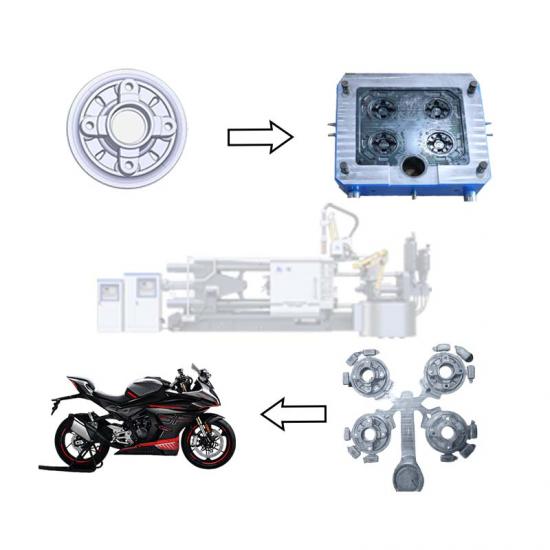
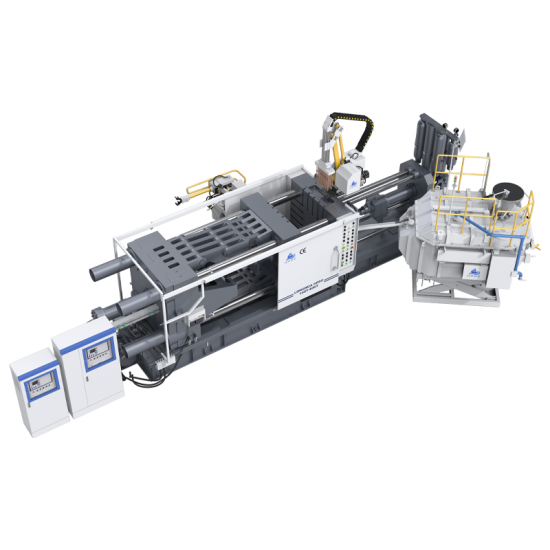
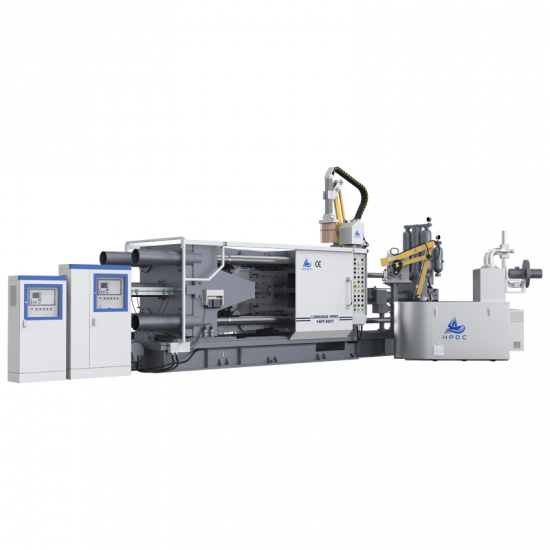
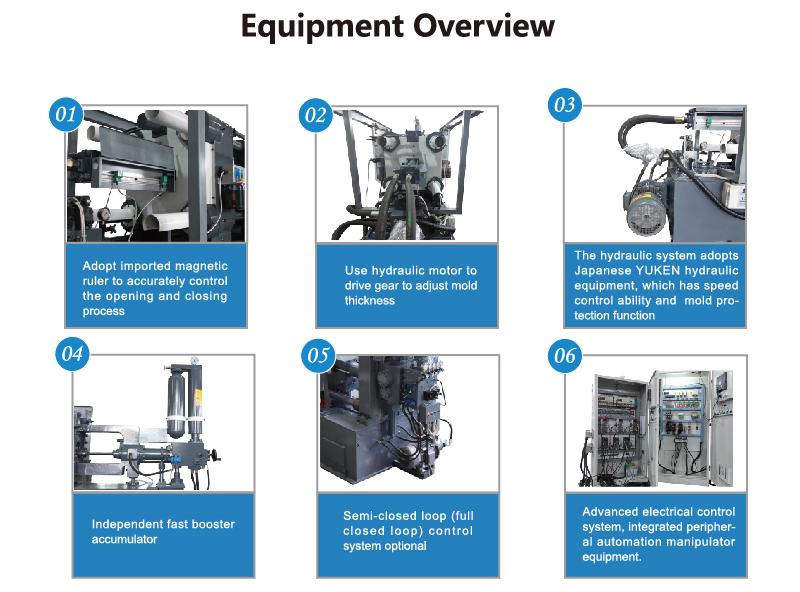
✅Finite element optimization of the fuselage, strong mold clamping rigidity, and not easy to expand the mold
The fuselage, head plate, second plate, and tail plate are made of integral cast steel + finite element stress simulation design. The Gorin pillars are high-strength chrome plating and tempered. The hinge structure is wear-resistant and fatigue-resistant. The clamping force output is uniform, and the template deformation is small during high-pressure injection. It effectively suppresses flash and material running, and is suitable for structural parts with large projection areas.
✅Independent energy storage high-speed injection system with controllable injection curve
It is equipped with independent fast injection and boosting accumulators, and is equipped with a magnetometer for fully closed-loop position feedback; the switching points of slow injection and fast injection, boosting pressure, and pressure building time can be accurately adjusted, with high injection repeatability, reducing air entrainment and pore defects, and supporting vacuum die-casting upgrades.
✅Servo energy-saving hydraulic system, stable consumption reduction
Servo main pump + imported hydraulic valve group, oil supply on demand, low power consumption in no-load standby, and stable oil temperature control; compared with traditional quantitative pumps, it saves 15%–25% of energy overall, has low oil temperature, and has longer life of oil seals and oil pipes, making it suitable for 24-hour continuous production.
✅Intelligent PLC human-machine control system, the process can be stored and traced
The independent industrial control touch screen can store hundreds of sets of mold process parameters; it has built-in fault self-diagnosis, production counting, cycle time recording, and process curve monitoring; the strong and weak current separation layout has strong anti-interference and supports docking with MES and remote operation and maintenance.
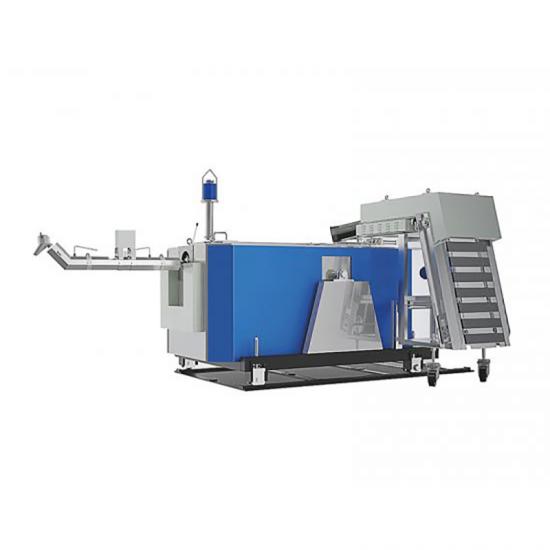
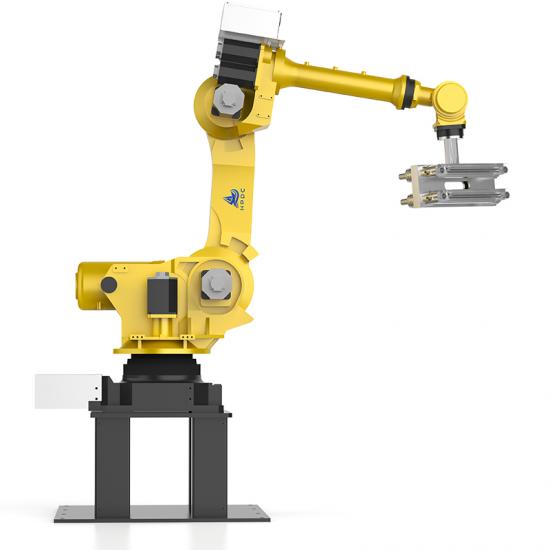
✅Modular expansion to adapt to automated die-casting units
Natively reserved manipulator, sprayer, soup machine, and vacuum device interfaces, with complete signal interlocking; it can quickly build a fully automatic die-casting island, and can also perform manual spraying and manual soup production on a single machine, and flexibly switch production modes.
✅Original one-stop package + localized technical services
Longhua complete machine + melting cup, ceramic injection head, hand-held spray gun, and complete supply of spare parts; engineers come to install the machine, adjust the machine, and provide operator training; support customized product-based lengthening injection, increased ejection force, and vacuum die-casting transformation plans.
Die casting machine working cycle
The die casting machine working cycle consists of six sequential steps. First, the movable platen moves forward to close and lock the mold. A measured amount of molten metal is then ladled into the shot sleeve by manual operation or an automatic ladling machine. Next, the plunger advances at low speed to seal the pouring opening and smoothly expel air from the shot sleeve, preventing air entrapment. Once the molten metal reaches the inner gate, the plunger accelerates and fills the die cavity at high speed before the metal solidifies. After the cavity is filled, the intensification system applies pressure to the solidifying metal, compensating for shrinkage and reducing porosity and shrinkage defects. Finally, after pressure holding and cooling, the mold opens, and the ejection mechanism pushes out the casting to begin the next cycle.
Product Parameters
|
LH series of standard parameter table (1250 T)
|
|
ITEMS
|
Unit
|
Specification
|
|
Clamping Force
|
KN
|
12500
|
|
Opening stroke
|
mm
|
1000
|
|
Die thickness(Min--Max)
|
mm
|
450~1180
|
|
Space between tie bars
|
mm
|
1100*1100
|
|
Ejector stroke
|
mm
|
200
|
|
Ejector force
|
KN
|
570
|
|
Injection position(0 as center)
|
mm
|
-160,-320
|
|
Injection force(intensification)
|
KN
|
1075
|
|
Injection stroke
|
mm
|
880
|
|
Plunger diameter
|
mm
|
¢100-¢140
|
|
lnjection weight(aluminum)
|
Kg
|
25.4
|
|
Casting pressure (intensification)
|
MPa
|
137/70
|
|
Max. casting area(40Mpa)
|
CM2
|
3125
|
|
Injection plunger penetration
|
mm
|
320
|
|
Diameter of pressure chamber flange
|
mm
|
240
|
|
Height of pressure chamber flange
|
mm
|
25
|
|
Max.working pressure
|
MPa
|
16
|
|
Motor power
|
Kw
|
30*2
|
|
Dimensions (L*W*H)
|
m
|
11.3*4.3*4.5
|
|
Machine lifting reference weight
|
T
|
80
|
|
Oil tank capacity
|
L
|
3000
|
(Note: We reserve the right to make any technical improvements without prior notice)
Company Introduction
Bengbu Longhua Die casting Machine Co., Ltd. is headquartered in Bengbu, Anhui — a time-honored industrial base and national transportation hub. We are a high-tech enterprise specializing in the design, R&D, manufacturing, sales, and global after-sales service of die-casting machines and supporting equipment.Founded in 1950 and entering die-casting machine R&D and production in 1982, Longhua is a pioneer in China's die-casting machinery sector, with decades of expertise driving continuous innovation and product upgrades.
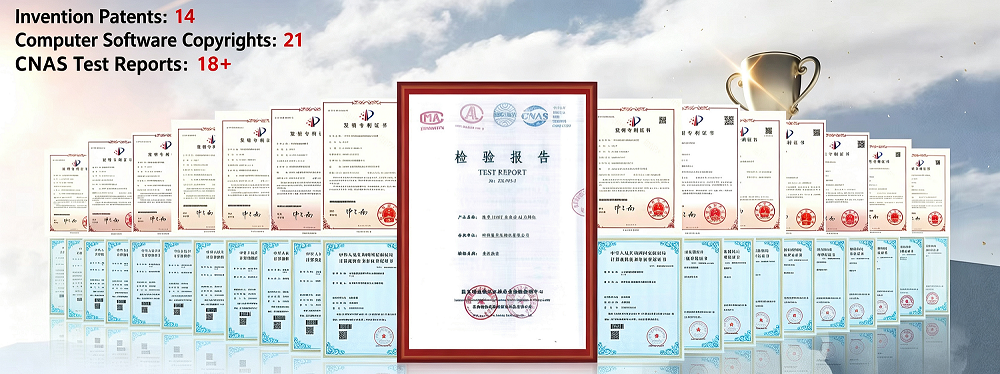
Our portfolio covers cold chamber and hot chamber die-casting machines, die-casting manipulators, industrial robots, and other auxiliary equipment, delivering integrated production solutions across diverse industries.We hold over 14 invention patents and 21 software copyrights, and lead the development of the group standard for the Artificial Intelligence Cold Chamber Die Casting Machine. Our products are backed by CNAS test reports and CE certificates for reliable quality compliance.
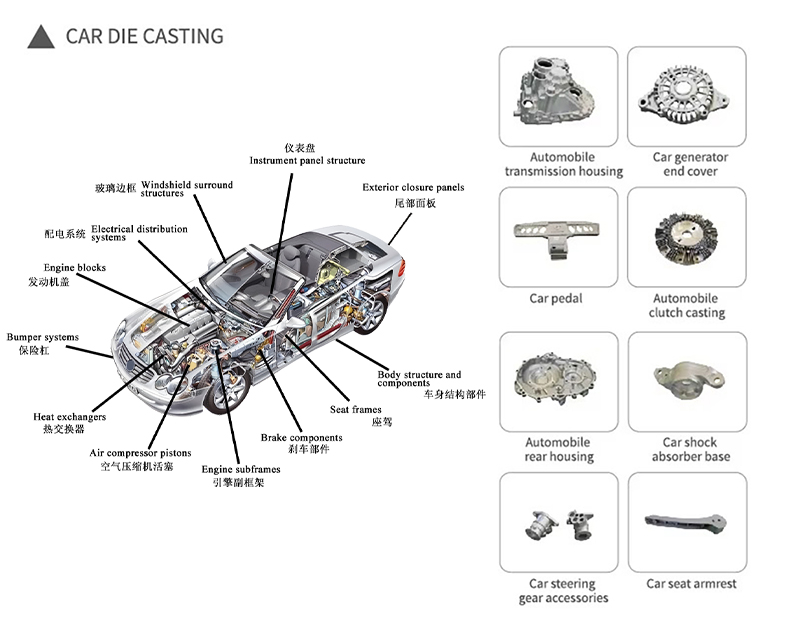
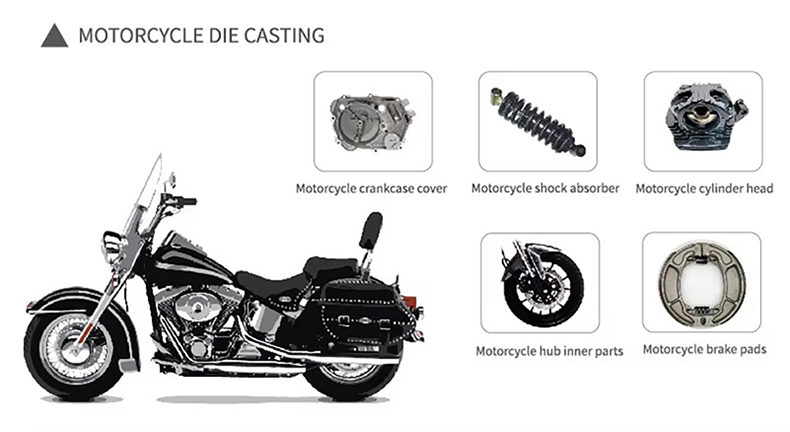
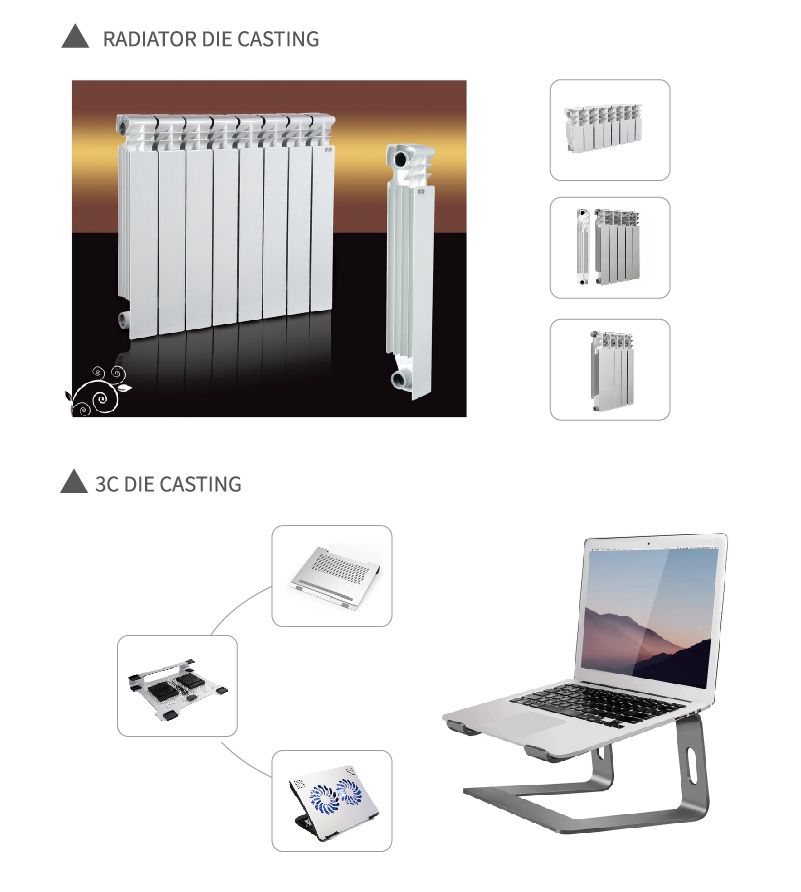
Our equipment has been exported to over 50 countries and regions, serving core sectors including automotive manufacturing, aerospace, and electronic information with stable performance and high production efficiency.
FAQ
Q1. How to choose between cold chamber die casting machine and hot chamber die casting machine?
Look at the alloy. The injection mechanism of the hot chamber machine is immersed in molten metal, which is suitable for low-melting point alloys such as zinc; the melting point of aluminum alloy is about 660°C, and the temperature of magnesium and copper alloys is higher. Long-term immersion will corrode the gooseneck and contaminate the casting, so cold chamber machines are often used. To put it simply: hot chambers are often chosen for small zinc parts, and cold chambers are chosen for higher melting point alloys such as aluminum, magnesium, and copper. The specific judgment depends on the product and batch size.
Q2. What is the difference between horizontal and vertical cold chamber die casting machines?
The horizontal machine mold opens and closes horizontally and the injection direction is horizontal, making it easy to connect to the manipulator for soup feeding, spraying, and picking up parts. It is the mainstream layout of batch workshops. The mold of the vertical machine opens and closes vertically, and the injection direction is vertical. It is more common in specific processes or heavy parts scenarios. Which one to choose first depends on the product, mold and workshop layout, not just the form.
Q3. How to calculate the tonnage (clamping force) of the die-casting machine? How big should I buy?
First calculate the total projected area of the parting surface (casting + runner + cake + overflow groove), and then multiply it by the selected boost pressure to get the required clamping force; when selecting, allow a margin for the working clamping force (usually about 60%–80% of the rated value). Do not estimate tonnage based on product weight. Give us the drawings and specific pressure requirements, and our technicians will review and recommend a model.
Q4. What are the functions of slow injection, fast injection and boosting?
Slow injection: The punch is pushed forward at a low speed to seal the pouring port, discharge the air from the pressure chamber smoothly, and reduce air entrainment. Fast injection: The molten metal accelerates after reaching the gate and fills the thin-walled cavity before solidifying. Pressurizing and maintaining pressure: After filling, pressurize the metal to compact it, feed it, and reduce pore shrinkage. The speed, position and pressure of the three stages are set according to the product process.
Q5. What are the benefits of servo hydraulics? Is it worth choosing?
The servo drive supplies oil according to action requirements, which can reduce no-load energy consumption, improve response speed and repeatability; the conventional hydraulic solution has a mature structure and straightforward maintenance. Whether the servo is equipped as standard is confirmed according to the model. Energy consumption and cycle time benefits need to be evaluated based on your production batch and shift.
Q6. Can it be equipped with automatic soup feeding, spraying, and pick-up equipment?
It can be matched according to the production line, or can be connected to the customer's existing peripheral equipment. It is necessary to confirm the equipment form, installation space, signal interface and action sequence during the planning stage; the interlocking and safety protection of the manipulator and the host must be planned together.
Q7. How to guarantee after-sales service and spare parts?
The warranty scope, period, response method and on-site/remote support are subject to the after-sales terms of the contract; the list of wearing parts and supply cycle are provided with the delivery materials. It is recommended to stockpile spare parts such as pressure chambers, punches, seals, and filter elements in conjunction with each shift.