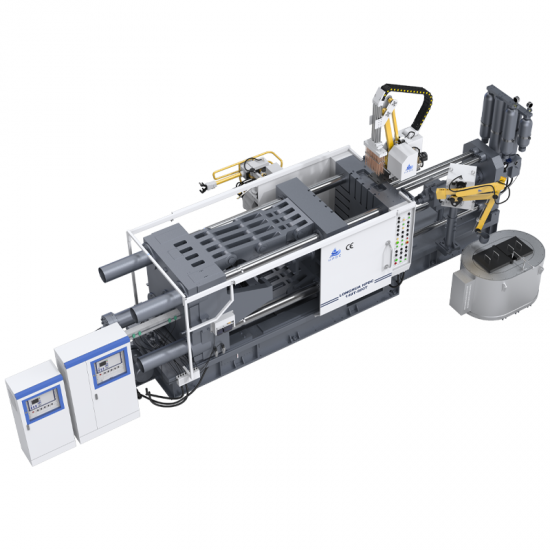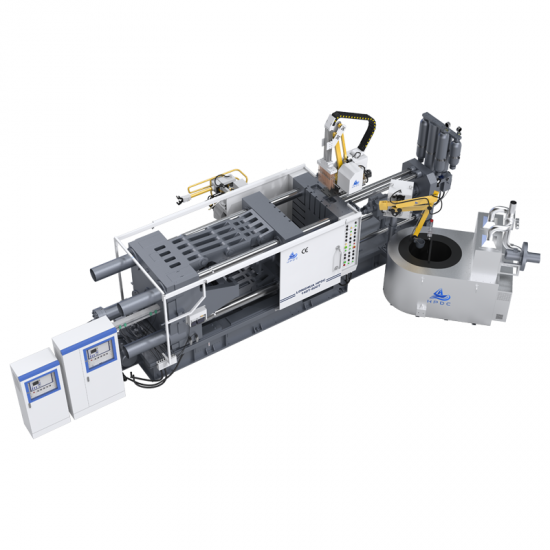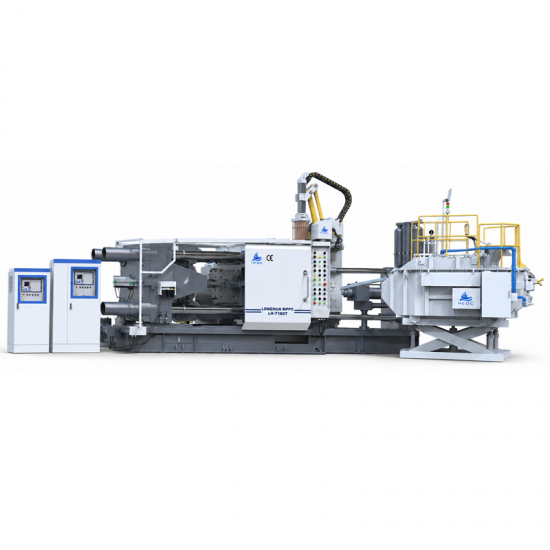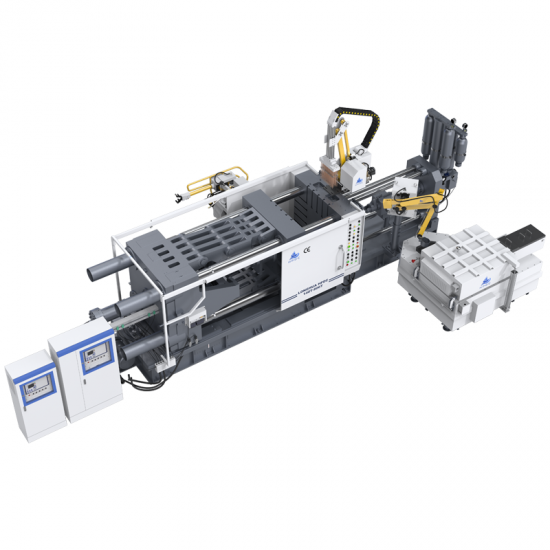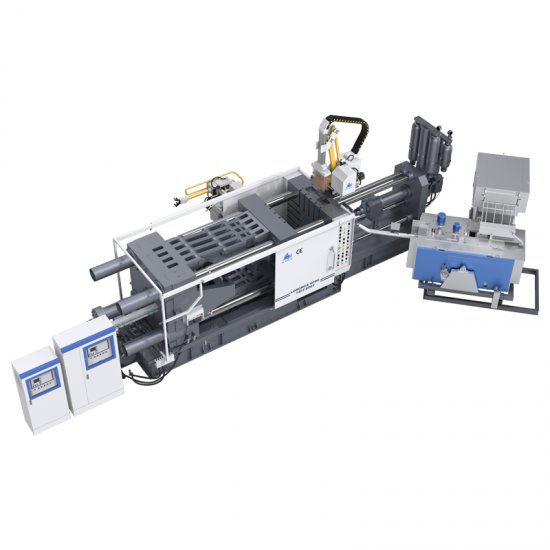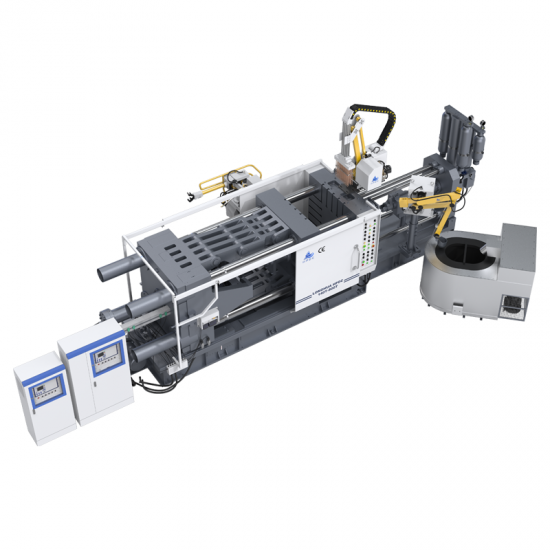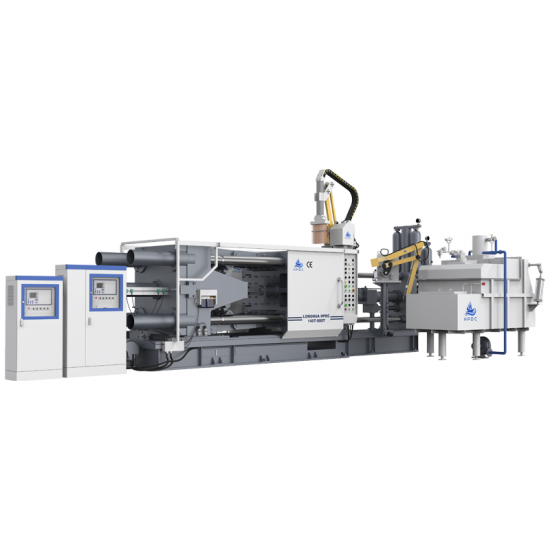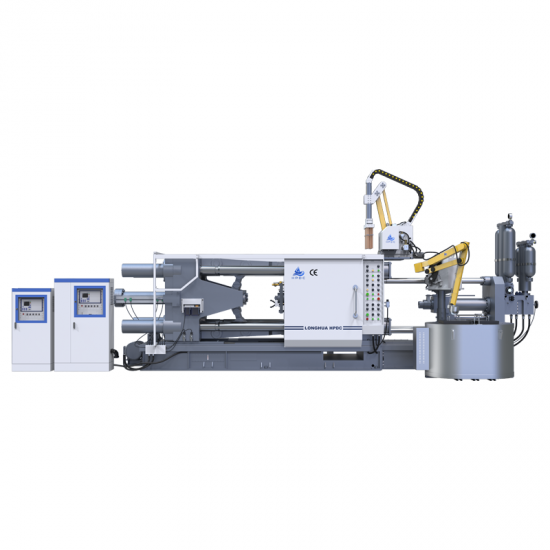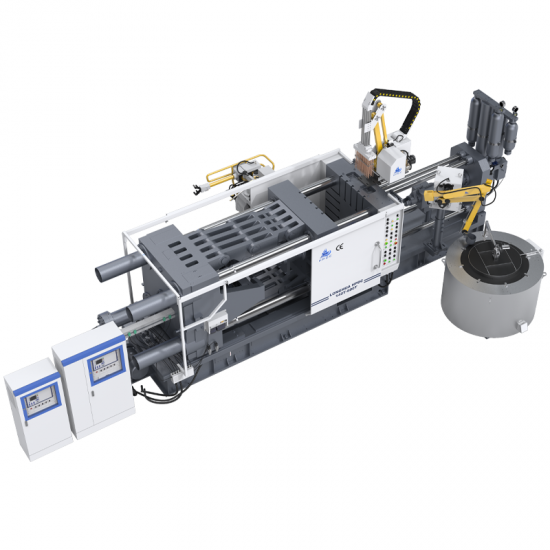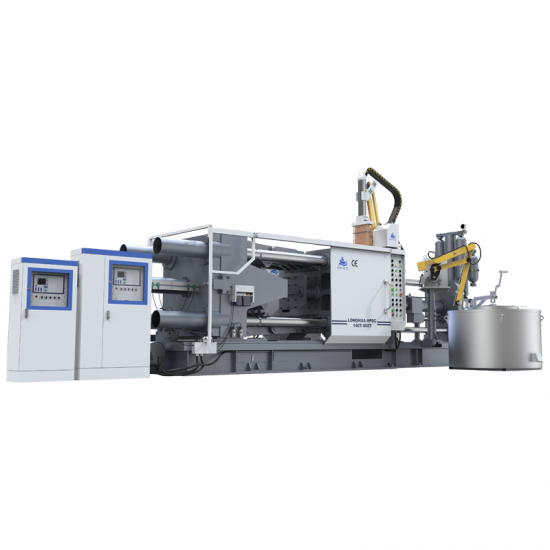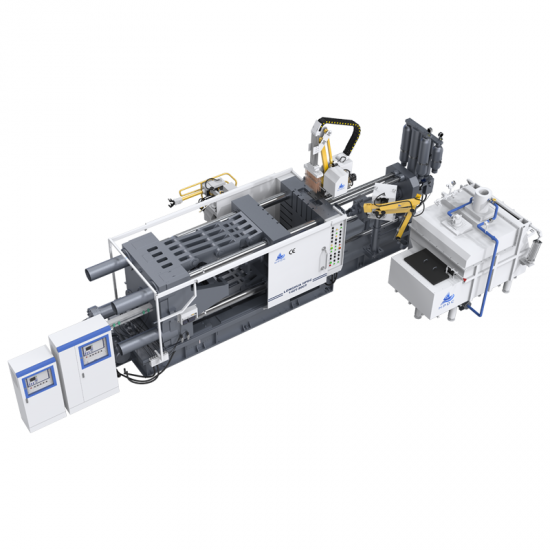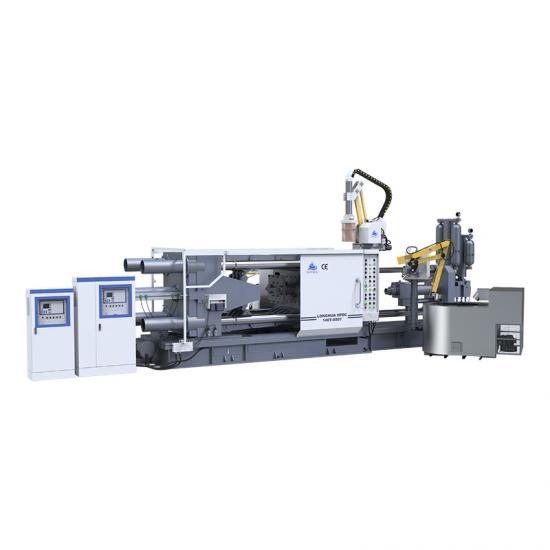




Core Selling Point
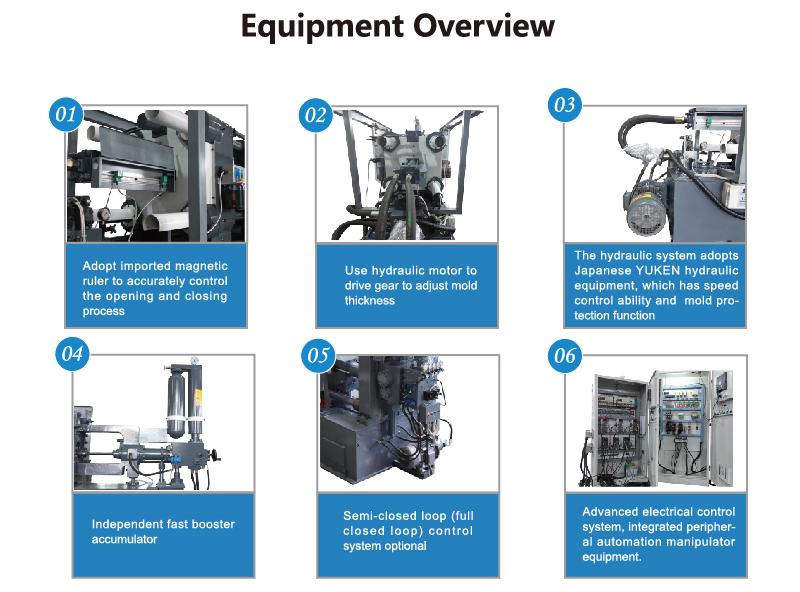
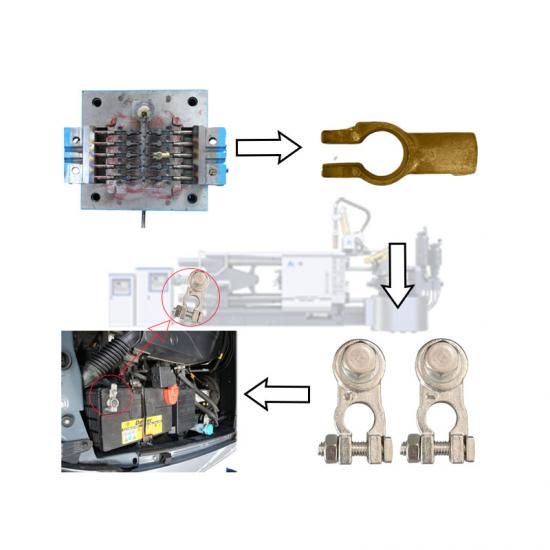
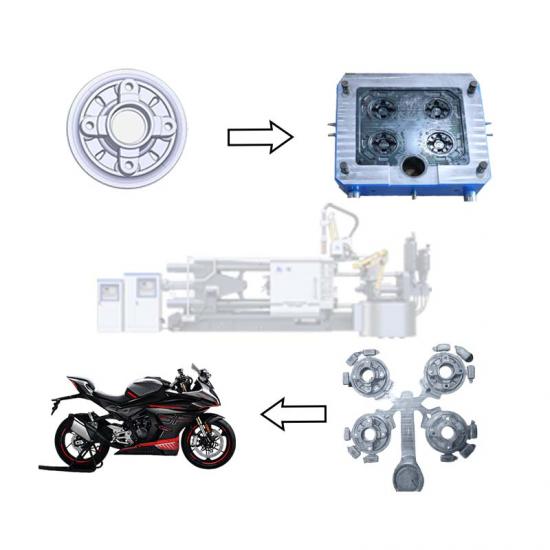
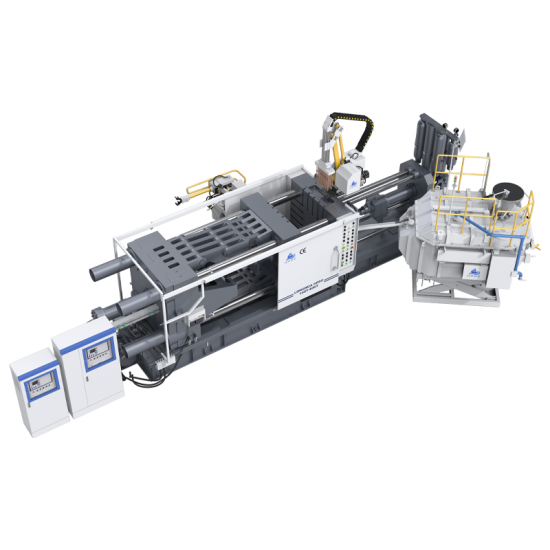
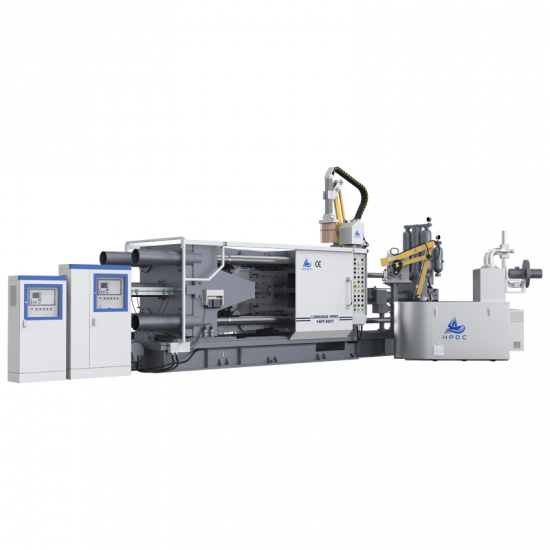
Die casting machine working cycle
- Mold closing: the movable template moves forward, and the mold is closed and locked.
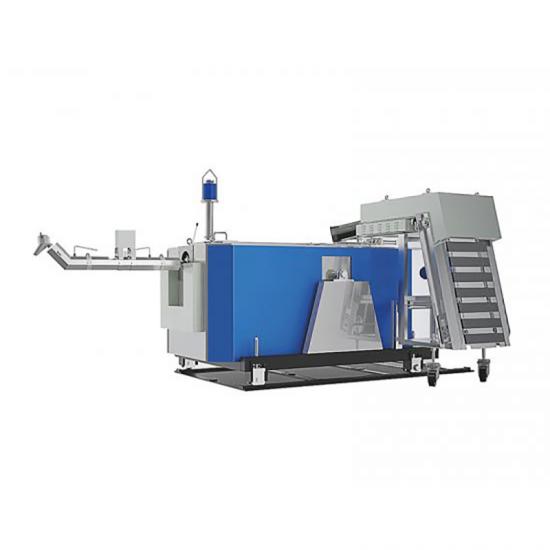
- Pouring: A certain amount of molten metal is scooped into the pressure chamber by manual or automatic soup feeding machine.
- Slow injection: The punch is pushed forward at a low speed to seal the pouring opening and smoothly discharge the air in the press chamber to avoid air entrainment.
- Rapid injection: After the molten metal reaches the inner gate, the punch accelerates and fills the cavity at high speed before the metal solidifies.
- Pressurization and pressure holding: After the cavity is filled, the pressurization system pressurizes the solidifying metal, shrinks it, and reduces pores and shrinkage porosity.
- Mold opening and ejection: After maintaining pressure and cooling, the mold is opened, and the ejection mechanism pushes out the casting to enter the next cycle.
Product Parameters
LH series of standard parameter table (2000 t)
ITEMS
Unit
Specification
Clamping Force
KN
20000
Opening stroke
mm
1400
Die thickness(Min--Max)
mm
650~1600
Space between tie bars
mm
1350*1350
Ejector stroke
mm
300
Ejector force
KN
650
Injection position(0 as center)
mm
-175,-350
Injection force(intensification)
KN
1510
Injection stroke
mm
960
Plunger diameter
mm
¢130-¢170
lnjection weight(aluminum)
Kg
40
Casting pressure (intensification)
MPa
113/66
Max. casting area(40Mpa)
CM2
5000
Injection plunger penetration
mm
400
Diameter of pressure chamber flange
mm
260
Height of pressure chamber flange
mm
30
Max.working pressure
MPa
16
Motor power
Kw
55*3
Dimensions (L*W*H)
m
13.5*4.7*4.8
Machine lifting reference weight
T
120
Oil tank capacity
L
3600
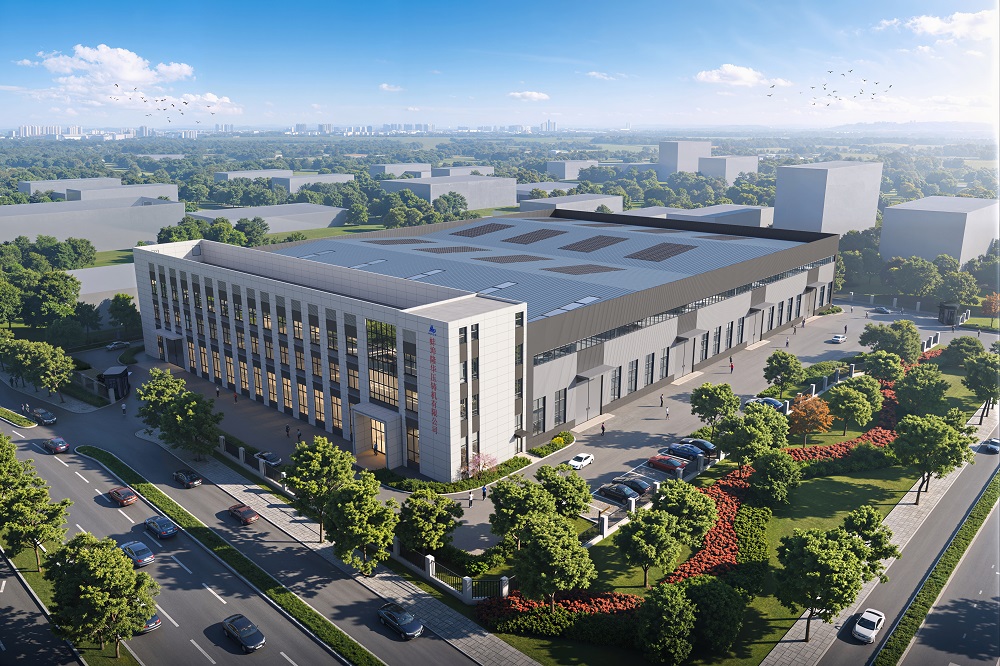
Bengbu Longhua Die-casting Machine Co., Ltd. is a high-tech enterprise located in Bengbu, Anhui, a traditional industrial base and national comprehensive transportation hub. Originating in 1950, we started die-casting machine R&D and manufacturing in 1982. As a pioneer in China’s die-casting machinery industry, we focus on continuous technological innovation and product iteration.
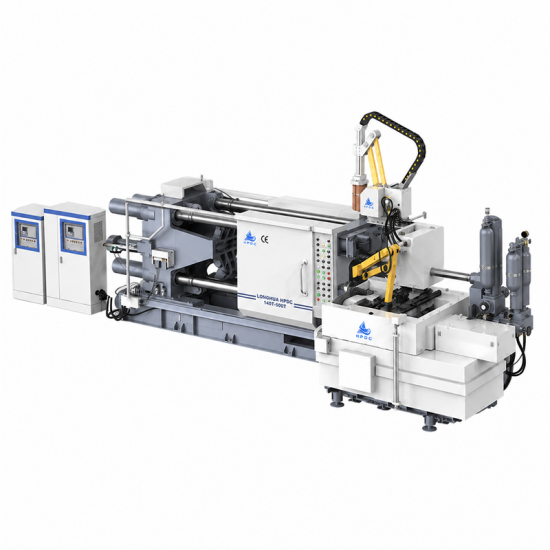
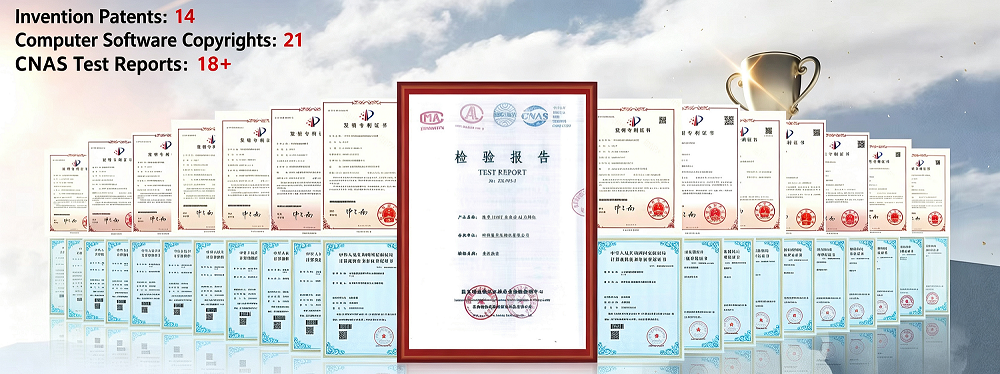
The company's product line has a complete layout. It mainly operates core machines such as cold chamber die-casting machines and hot-chamber die-casting machines. It is also equipped with die-casting manipulators, industrial robots and various die-casting auxiliary equipment. It has built a complete product matrix and can provide integrated die-casting production solutions to customers in different industries.We own more than 14 invention patents and 21 software copyrights, and lead the formulation of the group standard for Artificial Intelligence Cold Chamber Die Casting Machine. Our products hold CNAS test reports and CE certificates to ensure quality compliance.
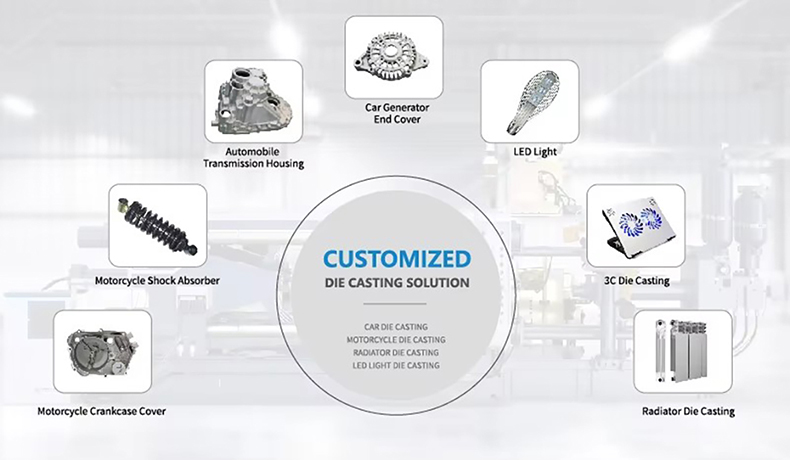
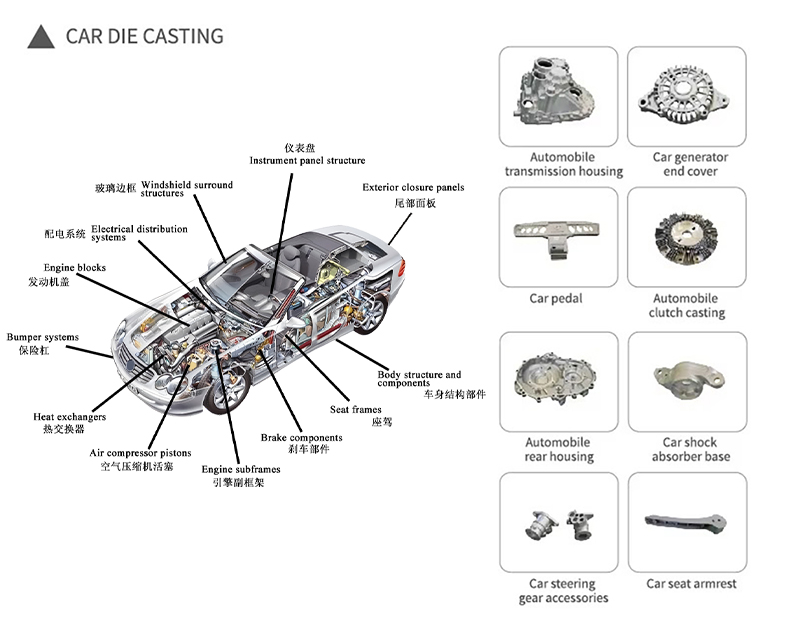
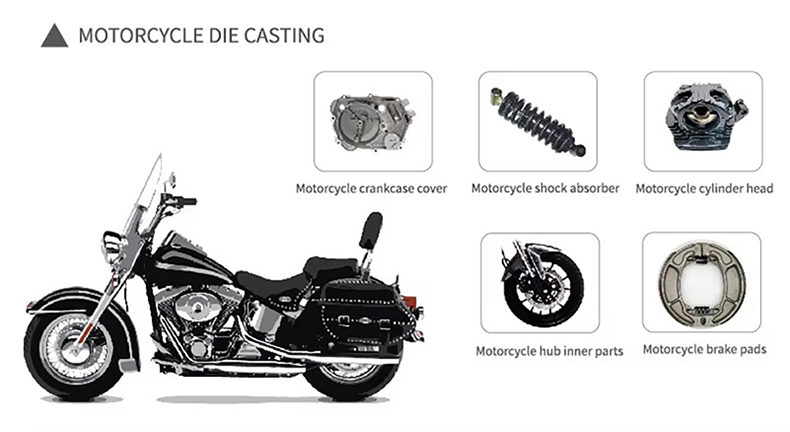
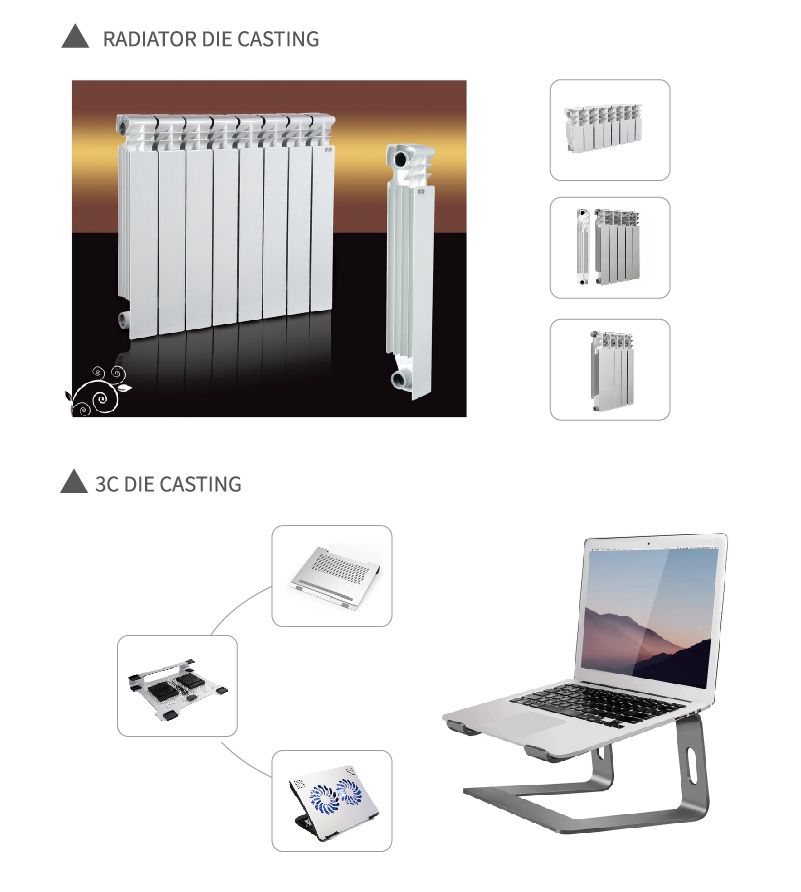
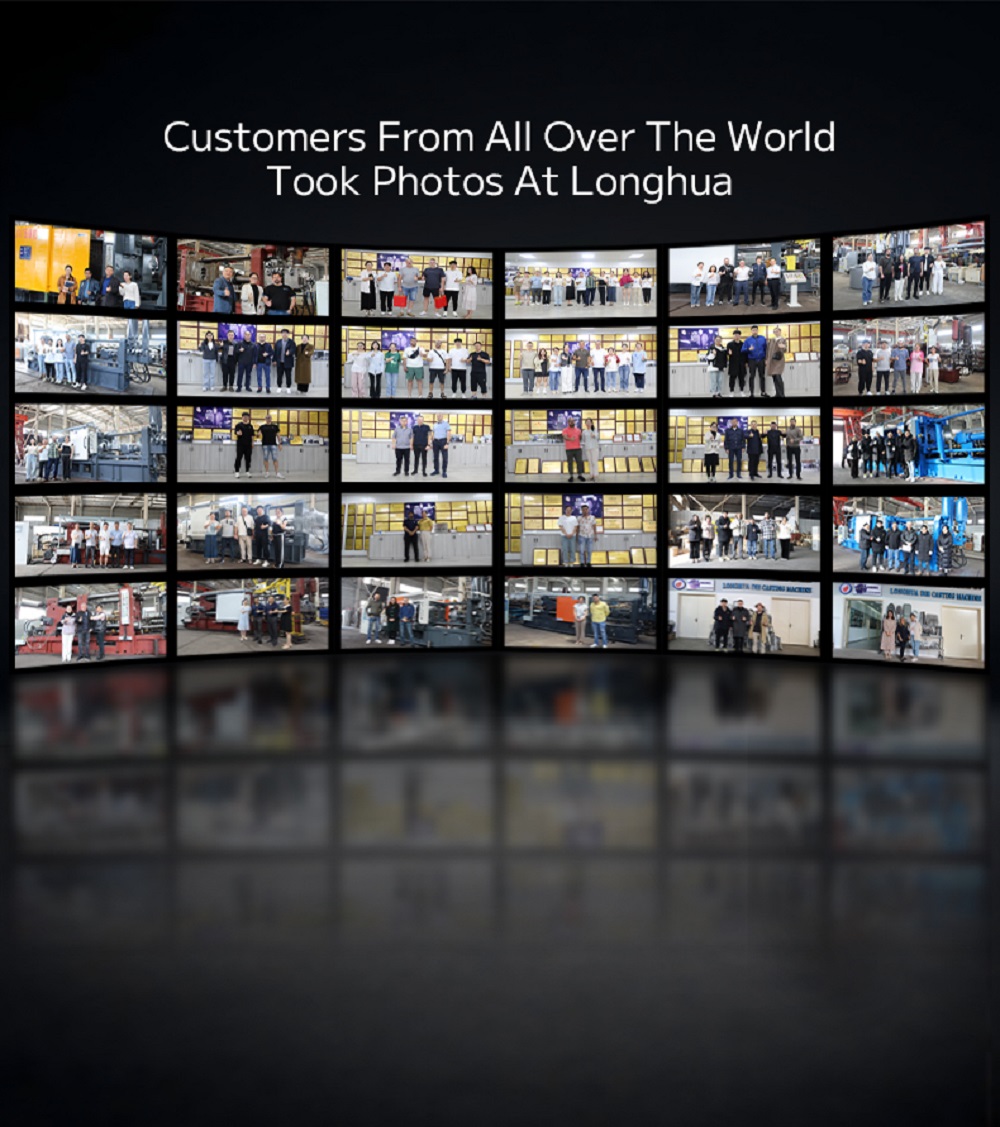
Our machines have been exported to over 50 countries and regions. With stable performance and high efficiency, they are widely applied in automotive, aerospace and electronic information industries, earning trust from customers worldwide.
FAQ
Q2. How to calculate the tonnage (clamping force) of the die-casting machine? How big should I buy?
First calculate the total projected area of the parting surface (casting + runner + cake + overflow groove), and then multiply it by the selected boost pressure to get the required clamping force; when selecting, allow a margin for the working clamping force (usually about 60%–80% of the rated value). Do not estimate tonnage based on product weight. Give us the drawings and specific pressure requirements, and our technicians will review and recommend a model.
Q4. Can cold chamber die casting machine be equipped with automatic feeding and robot pick-up?
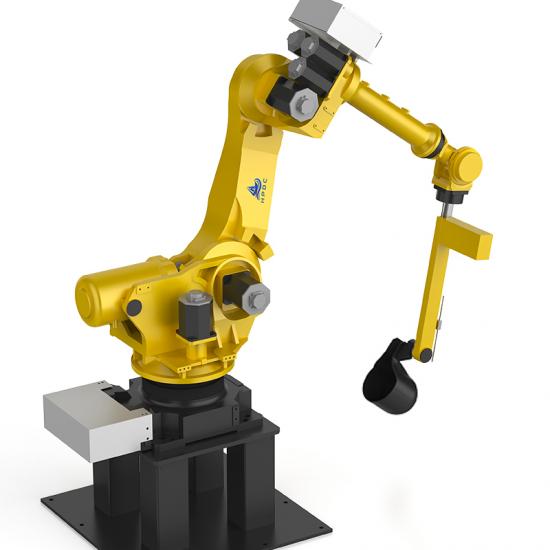
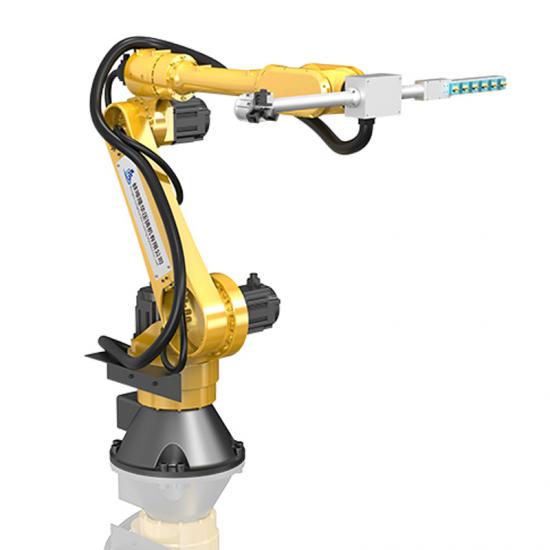
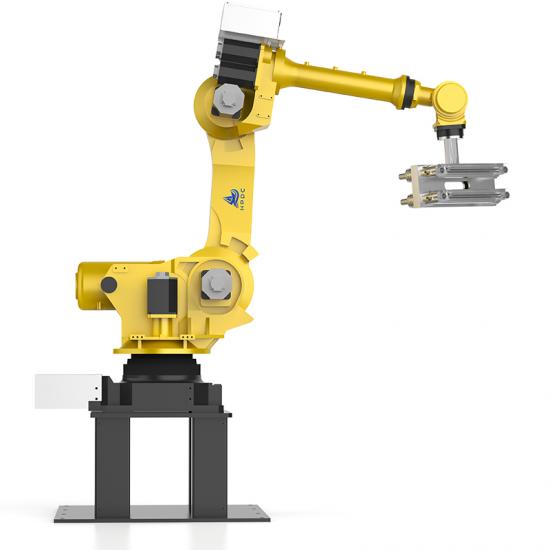
Yes. Most modern cold chamber die casting machines support integration with automatic ladling, spraying robot, pick-up robot and trimming station to form an automated die casting cell.
Q5. What common failure points of cold chamber die casting machine need regular inspection?
Shot piston and shot sleeve wear, injection accumulator pressure, clamping cylinder sealing, platen parallelism, safety limit switches, hydraulic oil cleanliness and cooling circuit.