Request a Quote
Language : English

English

  • Use of mold cooling system
    2021-04-14

    Use of mold cooling system

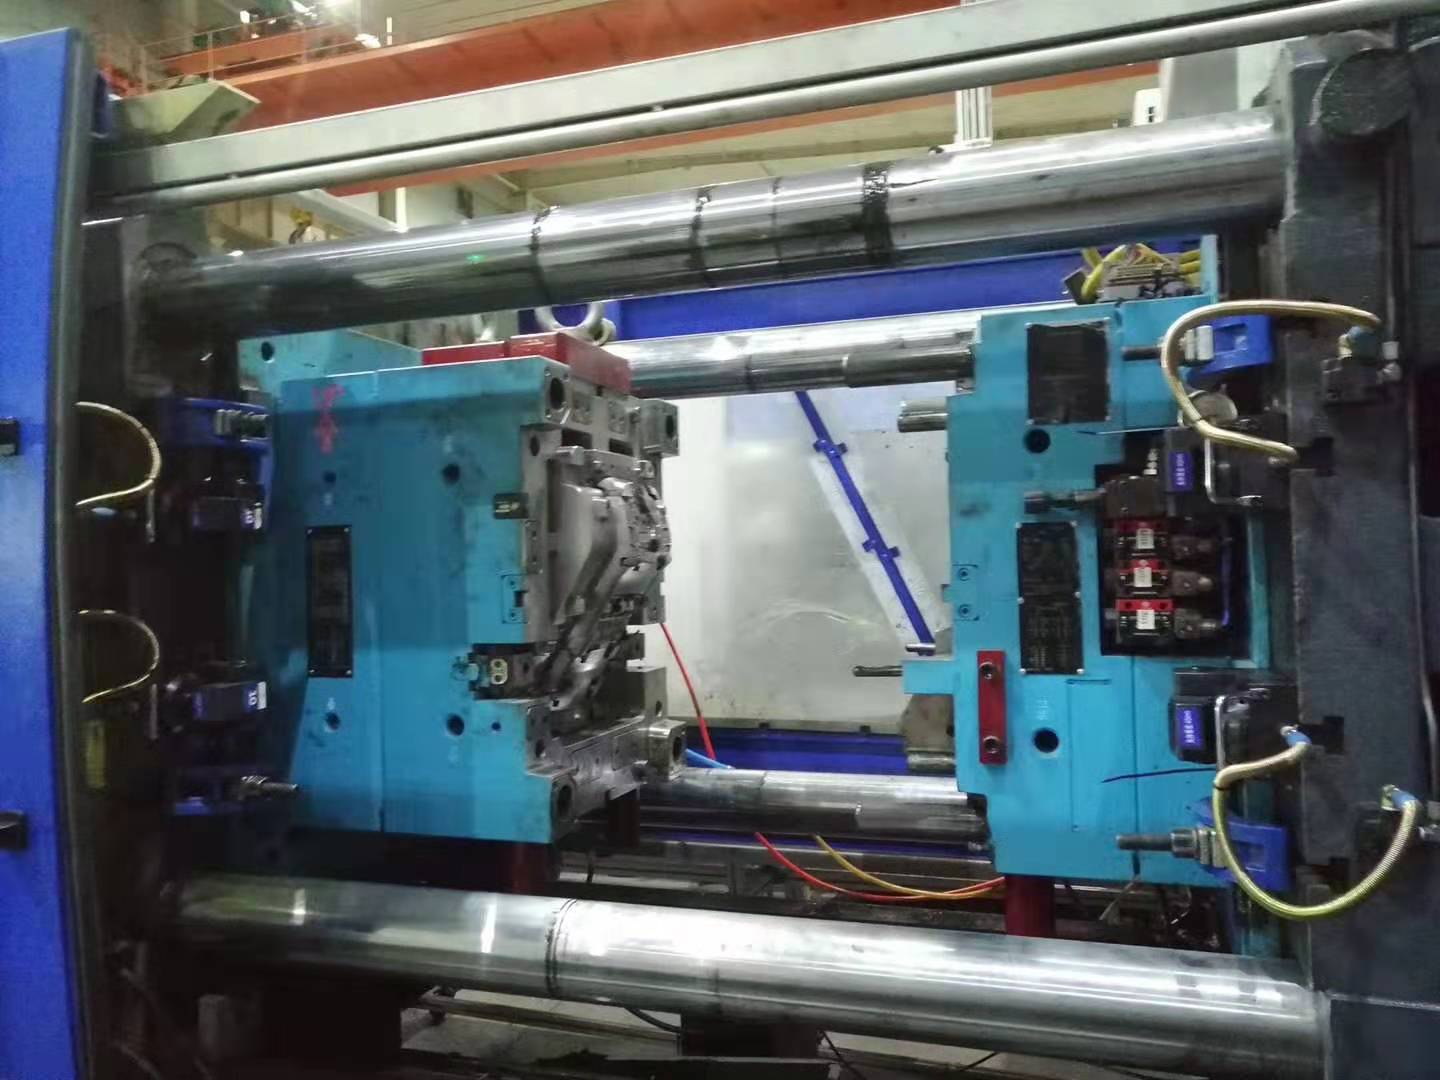
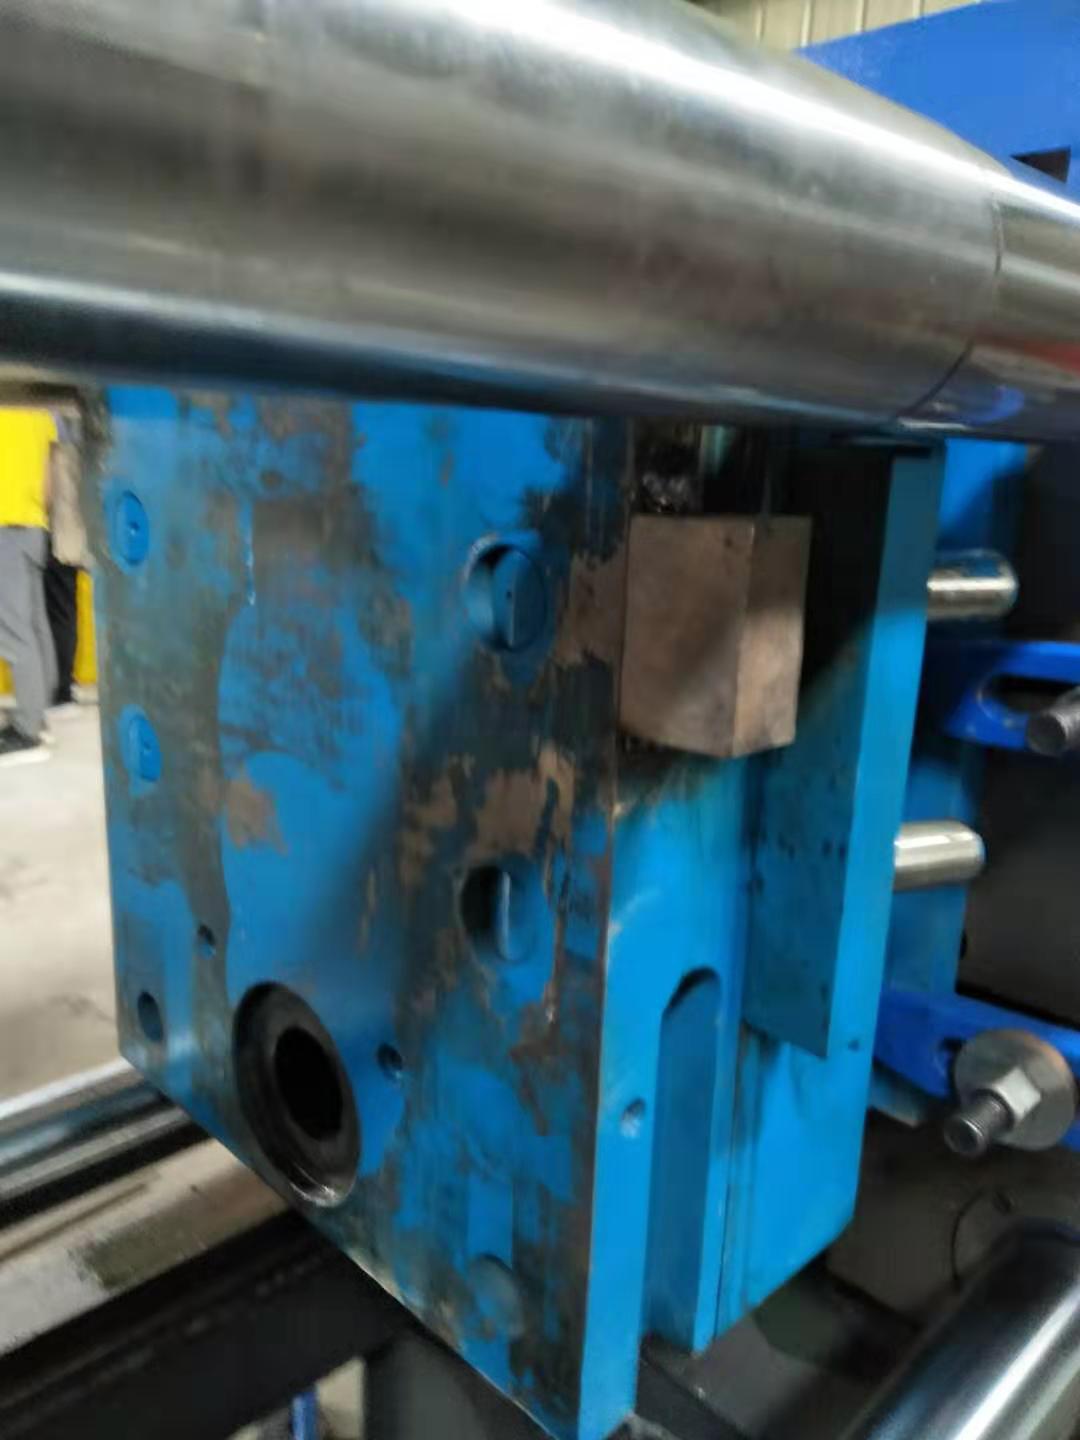
    In die casting, mold cooling is often ignored, but it is essential for extending mold service life and maintaining production efficiency. Many operators skip connecting cooling water pipes to save time, and some manufacturers even omit cooling channels to reduce costs, leading to serious unplanned downtime and early mold failure. Mold steel has its limits. When mold temperature is too high, the core surface develops early heat-checking cracks. Some molds show large-area cracking before reaching 2,000 shots. In extreme cases, core temperatures exceed 400°C, causing discoloration. Rapid chilling from release agent spray then worsens cracking, while castings suffer deformation, strain, soldering, sticking, or scrapping. Using a proper cooling water or oil system reduces release agent consumption and shortens spraying time. Benefits include shorter die casting cycles, better product quality, and fewer stoppages from mold cracking, strain, or sticking. Cooling also reduces wear on ejector pins, core pins, and mold cores, extending mold life and total output. However, cooling channels must be checked regularly for blockage. Blocked lines remove all benefits and recreate overheating problems. For die casting manufacturers, a reliable mold cooling strategy is a basic production requirement, not an option.
    Read More
  • Instruction after the operation of mold
    April 14,2021.

    Instruction after the operation of mold

    When temporary shutdown is required, the mold should be closed so that the cavity and core are not exposed to prevent accidental damage.Downtime is expected to be more than 24 hours, in the cavity, core surface should be anti-rust treatment, especially in the wet area and rainy season, even a short time to do anti-rust treatment.Because the moisture in the air will make the surface quality of the product quality.When the mold is used again, the grease spots on the mold should be removed and cleaned before use. When the production quantity of the mold has been completed and other molds need to be replaced, the following work shall be completed before the machine is shut down: 1.Turn off the cooling water first 2.Blow the excess water in the water channel of the mold 3.The oil in the cylinder used for core pulling should be emptied as far as possible and the oil nozzle should be sealed to avoid leakage of hydraulic oil or pollution of the surrounding environment during storage and transportation. 4.All moving parts, parting surface residual aluminum slag products or other foreign bodies must be removed clean, clean and on the product part, each moving parts, parting surface oil protection or spray anti-rust agent. 5.Fill in the relevant records truthfully, send the accessories of the mold to the maintainer, and attach the qualified products of the last mold to the inspector as samples
    Read More
  • Li Jun, Gai Yanbo, Cao Kai and other experts visited Longhua in Bengbu to inspect the progress of the cooperation project between the institute and enterprises.
    March 19,2021.

    Li Jun, Gai Yanbo, Cao Kai and other experts visited Longhua in Bengbu to inspect the progress of the cooperation project between the institute and enterprises.

    On March 17, Li jun, the municipal government deputy secretary-general and director of Bengbu Center, Caokai,one engineer of the intelligent mechanical department of Chinese Academy of Sciences institute in Hefei, conduct research and communication in the factory of the bengbu longhua die casting machine co., LTD.. The communication focused on the progress of the "high-speed and high -precision die-casting machine system " (this project was signed with Chinese Academy of Sciences, hefei institute in  the third China MEMS intelligent sensor industry development conference in 2019) At the meeting, Zhou Wenping, Head of the enterprise, said that after the research and development of Cao's engineer team, the die casting molding rate has been improved from 70.1% to 100%, and the operation was also more simple and more humane. Longhua has nine authorized invention patents. At present, its die casting machines has been exported to Russia, India, Pakistan, Vietnam, Turkey, Azerbaijan, Bolivia, Morocco and other countries, and it has won the unanimous praise of customers at home and abroad,. The sales volume of the products has also reached more than ten millions. Cao said that the second phase of the project began before Spring Festival , and the progress of the project is ahead of schedule. The two sides are now in negotiations on a new project "to replace the traditional Connecting rod manipulator with a robot.". Li stressed that Bengbu Center would fully support the upgrading and transformation of traditional manufacturing industry, what's more, encourage enterprises to cooperate with the Institute for scientific and technological innovation canter, to focus on the development opportunities and set up a long-term vision. While tracking and supervising the progress of the approved projects, the Center should also actively connect with new projects to help enterprises grow stronger and larger with the best quality services. Review of the signing ceremony between Bengbu Longhua and Hefei Institute of Chinese Academy of Sciences Production and research base site Invention patents (two of which were developed in cooperation with Hefei Institute of Chinese Academy of Sciences) "The mighty pass is like iron, and now I have crossed it from the beginning." "Let the world fall in love with Made in China"
    Read More
  • Nitrogen pressure requirements for die-casting machines
    March 16,2021.

    Nitrogen pressure requirements for die-casting machines

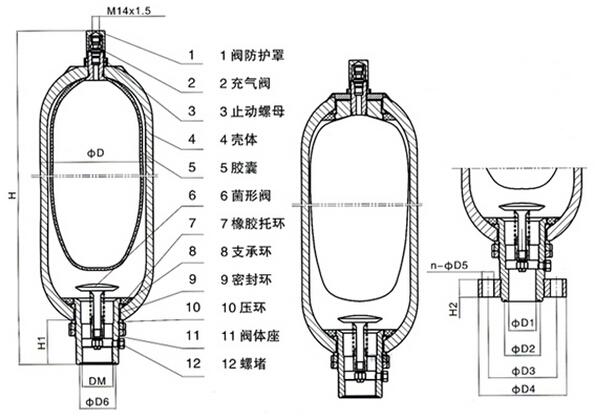
    (1) Within three days of the actual operation of the die casting machine, be sure to pay attention to check whether there is nitrogen leakage, so as to prevent the equipment from being damaged in the nitrogen bottle during transportation. (2)One week after the actual operation, the first inspection will be conducted. From then on, the inspection will be conducted once a week and then every two months. In case of insufficient pressure, nitrogen should be added in time. (3)Ways of examining the nitrogen pressure are as follows: close the operation of motor, stop switch calibration, open the pressure relief valve, at the same time, observe the hydraulic pressure of booster oil and 2 speed hydraulic pressure , when the oil pressure falls to zero, the two groups of accumulator nitrogen pressure value equal to the pressure accumulator nitrogen pressure and fast injection accumulator nitrogen pressure .The nitrogen pressure must conform to the standard value in the user manual.
    Read More
  • Reference for die casting process debugging
    2021-03-02

    Reference for die casting process debugging

    Bengbu Longhua Die Casting Machine Co., Ltd. releases professional technical guidelines on speed and pressure matching for precision die casting production, effectively solving common quality defects of thin-walled and thick-walled castings and optimizing the overall performance of die casting machine production. Compactness is the core standard for judging casting quality, and reasonable speed and pressure configuration is the key to stable production of high-quality die casting equipment. There are differentiated process logics for thin-walled and thick-walled die-cast parts. For thin-walled castings with high surface finish requirements, a fast injection velocity is essential, and conventional die casting machinery speed parameters can basically meet production standards. In contrast, thick-walled castings require both excellent surface quality and internal compactness, which cannot be satisfied by simple high-speed injection alone. After the two-speed nitrogen cylinder explosive injection, traditional machines often suffer from insufficient pressure supplement, resulting in loose internal casting structure and defective products. Speed and pressure present an inverse proportional relationship in die casting production, similar to vehicle gear operation: low speed delivers strong pressure, while high speed reduces thrust. To address the pain point of insufficient pressure for thick-walled parts, Longhua’s technical team has upgraded the independent supercharging function for its die casting machine. The optimized equipment balances injection speed and supercharging force, greatly improving the internal compactness of thick-walled castings and effectively making up for shrinkage holes and sprue sand holes caused by uncontrolled mold temperature. Professional equipment, high-precision molds and skilled operators are the three core elements of high-yield die casting production. The optimized speed and pressure matching technology perfectly adapts to diverse production demands of different wall-thickness castings, minimizes product defects, and helps global manufacturing enterprises achieve stable, efficient and high-quality intelligent die casting production.
    Read More
  • Matters needing attention in mold production
    2021-02-23

    Matters needing attention in mold production

    Bengbu LongHua Die Casting Machine Co., Ltd. has released standardized operational and maintenance specifications for die casting molds, delivering professional guidelines for safe and stable mass production with die casting machines. Standardized mold operation and daily maintenance are core foundations to avoid mold damage, reduce downtime, and improve the yield of precision die-cast products in industrial manufacturing. Before formal mold production, operators must follow strict pre-production rules.  1.Under cold mold conditions, shift handover or abnormal equipment status, workers need to reset switches and disable secondary injection and pressurization functions to prevent machine collision and die casting mold damage.  2.All casting residues and waste materials must be fully dried before putting into the crucible to avoid molten aluminum splashing and safety accidents.  3.Every die casting machine must be started with inching inspection, ensuring normal hydraulic oil temperature, lubrication and cooling water operation before formal production. In daily die casting production, standardized process control is essential, including professional mold spraying, sliding part oil brushing, and thorough cleaning of aluminum slag and foreign matters on parting surfaces. Operators must strictly control material temperature and mold temperature via mold temperature machines and cooling systems, and adjust handle thickness and process parameters according to product quality conditions. For long-term service life of die casting molds, workers must clean cavity surfaces, exhaust slots and overflow tanks regularly with air guns or copper rods instead of hard tools to avoid cavity scratches. Regular mold cleaning with professional oil agents removes corrosive compounds, prevents surface dulling and ensures stable casting quality. Besides, it is necessary to fasten mold components, check slider limits and record product quality regularly, realizing scientific full-lifecycle die casting mold maintenance and maximizing production efficiency.
    Read More
  • Cold mold production plan
    2020-02-16

    Cold mold production plan

    1. Basic Operation Standards for Cold Mold Startup The mold in the cold mold state, to brush more oil, less spray. When the mold temperature reaches the technical requirements after the normal spray coating. Then the two blocks and pressurized gradually open, and according to the normal process of production. 2.Low-Pressure Pre-Production Debugging Process Mold in the case of no preheating to low-pressure production, and the production parameters on the machine must be reduced or closed to zero (remember: do not open fast injection to prevent mold run and stick).Every production of a mold to brush the oil or demoulding paste, to prevent the cold mold adhesion with material phenomenon (aluminum temperature had better reach 680℃ above, so the mold temperature rise faster).Low pressure production of about 30 molds, with the exhaust device and injection in each mold to close the exhaust valve in time, at the same time to observe the normal operation of the active parts, and then debug the production parameters of the machine until the production of qualified products and extraction of finished products.In the die casting production, it is found that the gate and the casting parts have the phenomenon of aluminum sticking pull caused by impact.If there is running material, should be cleaned up in time, otherwise the more tight the pressure, the more difficult to clean up. 3. Cold Mold Production Inspection & Formal Production Switching Standards After completing low-pressure trial production and parameter debugging, conduct comprehensive inspection on casting appearance, internal porosity and surface finish. Operators need to continuously monitor mold temperature changes and keep the release agent coating uniform and moderate to avoid insufficient lubrication or residual oil gas defects. When the mold temperature is stable within the standard production range, no sticking aluminum, flash, pulling and other abnormal defects appear in continuous 50 qualified castings, and all mechanical moving parts operate smoothly without jitter or stalling, the production line can be officially switched to normal high-efficiency mass production mode.
    Read More
  • The correct preheat production plan of the mold
    2021-02-09

    The correct preheat production plan of the mold

    The correct preheat production plan of the mold 1.If the die casting mold needs to be preheated before production, the cooling water of the mold shall be temporarily closed, and then the water volume shall be gradually adjusted according to the mold temperature. When preheating the mold, be careful not to make the mold local overheating (dark red phenomenon), in case the mold annealing. 2.When preheating the mold, it is forbidden to use two-block injection or pressurized injection.It must be heated effectively without damaging the mold according to the design requirements of the mold.For those with thermostatic tubing, use a mold temperature controller for heat preservation and heating.If there is no thermostatic tubing, gas can be used to increase the temperature. When heating, it should be done gently, evenly and slowly so that the temperature rise of the core and the core seat can be synchronized with the expansion.When the mold temperature preheats to about 220°, run each moving part to prevent the normal operation from being affected by the phenomenon of tight biting due to thermal expansion.After producing about 10 molds at low pressure, the high pressure production parameters were adjusted and qualified products were extracted.In the early stage of die casting production, it was found that the sprue part and the casting part of the finished product had the phenomenon of aluminum sticking pull caused by impact.If there is running material, should be cleaned up in time, otherwise the more tight the pressure, the more difficult to clean up.
    Read More
first page 21 22 23 24 25 26 27 28 29 30 last page

A total of 37 pages

leave a message leave a message
If you are interested in our products and want to know more details,please leave a message here,we will reply you as soon as we can.
Home

Products

News

Contact