Request a Quote
Language : English

English

  • Basic Principles of Die Casting
    2021-07-06

    Basic Principles of Die Casting

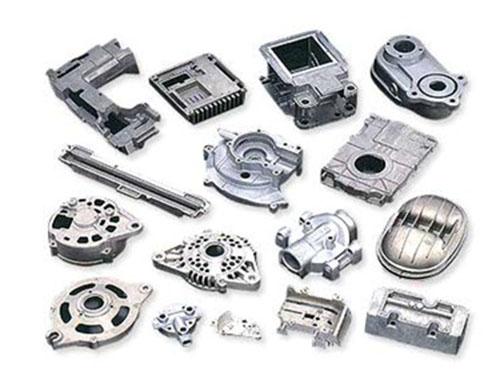
    1. Consider the injection pressure: multi‑stage injection with different functions There are four stages for injection pressure: fast pressure, filling, pressurization, and pressure holding, each with distinct functions. In the initial phase, the piston pushes molten metal into the cavity at a relatively low speed until the cavity is fully filled. Pressure holding stage:The injection punch transmits pressure to the cavity via the solidified residual material and the metal at the junction. This enables the solidifying metal to crystallize under pressure, producing castings with dense internal structure. The duration of pressure holding is mainly determined by die‑casting alloy properties, casting wall thickness, gating system and other working conditions. Cooling stage:The cooling stage covers the time from the end of pressure holding until the casting is ejected in the die‑casting cycle. Filling time:Adjust die‑casting filling time according to product geometry and wall‑thickness variation. 2. Critical die‑casting process parameters affecting casting quality Multiple parameters exert great influence on final casting quality: Residence time of molten alloy inside the shot sleeve Punch speed or punch acceleration at the start of the first‑shot phase Transition point from first‑shot to second‑shot phase (displacement stroke for each injection stage) Punch acceleration time and filling time during the mold‑filling (second‑shot) phase Boost pressure and boost time for molten metal inside cavity after filling completion Solidification time of castings within the mold cavity Derived core die‑casting process specifications include: slow injection speed, high‑speed (mold‑filling) speed, speed‑switch position, boost pressure, and cooling time. Slow injection speed:Slow injection speed should be properly controlled to avoid turbulence of molten alloy inside the shot sleeve and excessive temperature drop of molten metal. The advanced 9‑stage low‑speed control is widely adopted nowadays. It simulates uniformly‑accelerated motion and minimizes gas entrapment inside the shot chamber. High‑speed speed (secondary speed):Also known as secondary speed, it refers to punch speed during mold filling. Proper control ensures favorable atomized metal flow at the ingate during cavity filling. Reference values shall be selected based on casting structure and wall thickness, then converted into punch travel speed according to ingate dimension and shot‑chamber size. Speed‑switch position:Also called second‑speed switch position, it defines where the punch begins to accelerate. Acceleration can be triggered when the shot sleeve is fully filled, when molten alloy reaches the ingate, or after partial cavity filling. This position must be fine‑tuned according to product features and actual production defects. Boost parameters (four controllable factors):Four parameters should be managed for boost function: Start position of pressurization Pressure building time Pressure holding ...
    Read More
  • Bengbu LongHua Launches High-Efficiency Energy-Saving Die-Casting Machine, Empowering Global Manufacturers with Significant Cost Reduction and Quality Upgrade
    2021-06-25

    Bengbu LongHua Launches High-Efficiency Energy-Saving Die-Casting Machine, Empowering Global Manufacturers with Significant Cost Reduction and Quality Upgrade

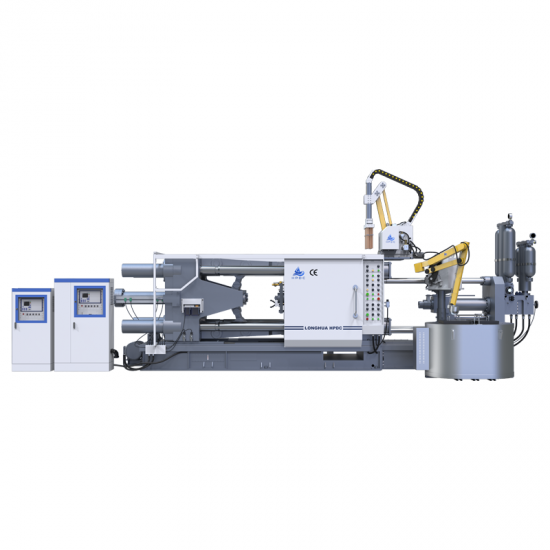
    BENGBU, China – September 1, 2026 — Bengbu LongHua Die Casting Machine Co., Ltd., a national high-tech enterprise and standard setter for China’s intelligent die-casting industry, has unveiled its self-developed intelligent high-speed and high-precision energy-saving die-casting machine. Co-developed with the Hefei Institutes of Physical Science, Chinese Academy of Sciences, the patented equipment delivers comprehensive upgrades in energy conservation, production efficiency, product qualification rate and service life, providing highly cost-effective intelligent manufacturing solutions for global die-casting enterprises. LongHua’s flagship energy-saving die-casting project was officially launched at the 3rd China MEMS Intelligent Sensor Industry Development Conference in November 2019, supported by the Anhui Provincial and Bengbu Municipal governments. Listed as one of Bengbu’s four core high-end manufacturing projects, the equipment boasts 9 national invention patents, 33 utility model patents, 2 high-tech product certifications, 1 Anhui Provincial New Product Certificate and 4 software copyrights, owning completely independent intellectual property rights. Against the backdrop of rising global industrial energy consumption and production costs, LongHua’s new-generation die-casting machine solves core pain points of traditional casting equipment with eight major competitive advantages, realizing all-round cost reduction and efficiency improvement for manufacturers. In terms of energy saving and cost reduction, compared with mainstream same-tonnage die-casting machines from other domestic brands, LongHua equipment achieves a50%-80% power saving rate. Based on 24-hour continuous production, 30 days a month, it saves 10,800 kWh of electricity monthly, equivalent to an annual electricity cost saving of 129,600 CNY, greatly reducing enterprises’ daily operation expenses. The equipment features an innovative hydraulic oil temperature reduction technology, lowering operating oil temperature by about 8°C during production. This optimization extends the service life of core components including hydraulic valves, pumps, valve plates, hydraulic oil, molds, injection chambers and plunger heads by 40%, and reduces overall production costs by approximately 40% compared with peer products. In terms of production quality, the full closed-loop energy-saving hydraulic system achieves ultra-precise control of system pressure and flow. It effectively raises the qualification rate of die-casting products, eliminating the massive energy, consumable, labor and cycle waste caused by the 70% qualification rate of traditional equipment. Meanwhile, the optimized pump station structure accelerates the machine’s response speed, boosting overall production efficiency by 30% than ordinary die-casting machines. The equipment also realizes comprehensive environmental and operational upgrades. It reduces operating noise by more than 6 decibels, greatly improving the workshop wor...
    Read More
  • Do you know the cycle of die casting molds?
    2021-06-18

    Do you know the cycle of die casting molds?

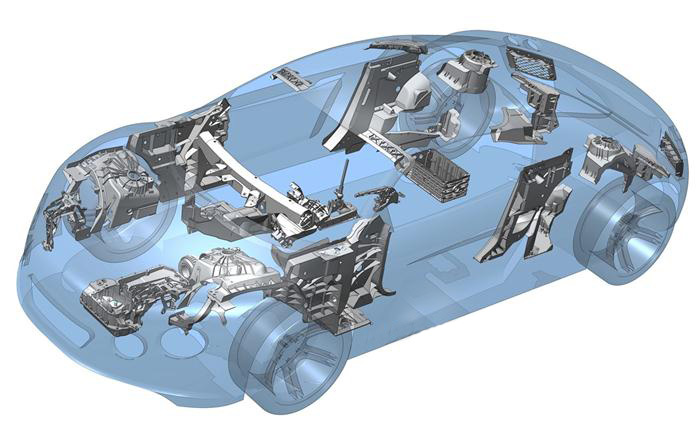
    Metal die-casting is an advanced technology with less and no cutting. It has the characteristics of high consumption efficiency, saving original materials, reducing consumption costs, good casting performance, and high precision. It is widely used. Among them, the largest market for die-casting castings is the automotive industry. As humans pay more and more attention to sustainable development and environmental maintenance, automotive lightweighting is the best way to achieve high efficiency, safety, energy saving, warmth and environmental protection. Using aluminum alloy instead of traditional steel to make cars can reduce the weight of the whole car by about 30%. Because the die-casting mold is to die-cast molten metal at 400~1600℃ under high pressure (30~150MPa). During the molding process, the mold is periodically heated and cooled, and is scoured and corroded by hot metal sprayed at high speed. Mold materials require high thermal fatigue resistance, thermal conductivity, and good wear resistance, corrosion resistance, and high temperature mechanical properties. It is still difficult to meet the ever-increasing performance requirements only by the application of mold materials. Various surface treatment technologies must be applied to the surface treatment of die-casting molds to meet the requirements for high efficiency, high precision and long life of die-casting molds. Die-casting mold failure method When the die-casting mold is in contact with high-temperature liquid metal, it not only has a long time of heating, but also the heated temperature is higher than that of forging dies. The temperature of die-casting non-ferrous metals is 300~800℃, and the temperature of die-casting ferrous metals is above 1000℃. It also received a very high pressure of 30-150 MPa, and was subjected to wear and corrosion caused by repeated heating and cooling and high-speed scouring of liquid metal activities.
    Read More
  • Sales of new energy vehicles increasing sharply, and aluminum alloys usher in new opportunities
    2021-06-01

    Sales of new energy vehicles increasing sharply, and aluminum alloys usher in new opportunities

    The rapid development of the new energy vehicle industry has created huge market opportunities for the aluminum die casting machine sector, driving continuous upgrading and innovation of global die casting equipment. Though new energy vehicle technology is still evolving, its core advantages in energy saving, emission reduction and environmental protection ensure long-term industrial growth, bringing unprecedented development momentum to the die casting machinery manufacturing industry. Driven by national energy conservation policies and financial subsidies, the new energy vehicle market has achieved explosive growth. Industry data shows that new energy vehicle sales exceeded 1.03 million units before November 2018, with a year-on-year increase of 68%, marking the official takeoff of the domestic new energy automotive market. This booming trend greatly boosts market demand for high-performance aluminum die casting machine, as aluminum alloy has become the core lightweight material for new energy vehicles. Aluminum alloy features low density, light weight, excellent corrosion resistance, high plasticity and stable strength, perfectly meeting the lightweight manufacturing needs of new energy vehicles. It is widely applied in auto bodies, engine parts, chassis, suspensions, wheel hubs, heat exchangers and battery components. With expanding aluminum alloy application scenarios, the market demand for precision die casting equipment continues to surge. However, aluminum alloy processing faces technical challenges compared with traditional steel processing. Complex processing techniques raise production difficulties, and unqualified casting processing will affect vehicle safety and stability. As a professional die casting machinery manufacturer, Longhua focuses on optimizing aluminum die casting technology and equipment performance. It provides high-precision, stable aluminum die casting machine solutions for automotive lightweight production, helping the new energy vehicle industry achieve high-quality and sustainable development.
    Read More
  • Eid Mubarak to all Muslim friends!
    2021-05-14

    Eid Mubarak to all Muslim friends!

    Eid Mubarak to all Muslim friends!  عيد سعيد عيد مبارك  السلام عليكم ورحمة الله وبركاته،  تقبل الله صيامكم واعمال الصالحين و عيد سعيد وعمر بالخير  وكل عام وانتم والاسرة الكريمة بخير  开斋节吉庆!恭祝各位身体安康!家庭和睦!万事顺遂!
    Read More
  • Bengbu Longhua warmly congratulates the successful opening of the 2021 China (Anhui) Science and Technology Innovation Achievement Transformation Fair!
    2021-05-06

    Bengbu Longhua warmly congratulates the successful opening of the 2021 China (Anhui) Science and Technology Innovation Achievement Transformation Fair!

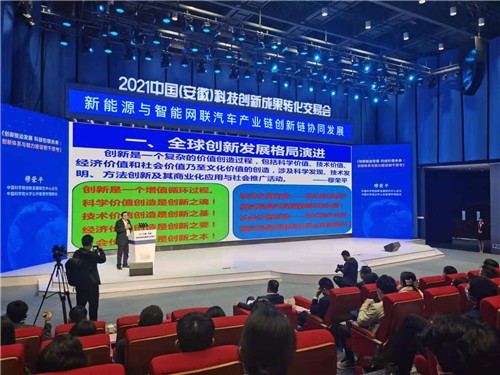
    On the morning of April 26, the opening ceremony of the 2021 China (Anhui) Technology Innovation Achievement Transformation Fair was held in the Anhui Innovation Hall. Zhang Qingli, vice chairman of the National Committee of the Chinese People's Political Consultative Conference, delivered a speech and announced the opening of the fair. With the theme of "Consolidating the Foundation of Innovation and Accelerating the Transformation of Scientific and Technological Achievements", this session of the Science and Technology Fair is co-sponsored by the Ministry of Science and Technology of China, the Chinese Academy of Sciences, and the Anhui Provincial People's Government.  Li Jinbin, Secretary of the Anhui Provincial Party Committee and Director of the Standing Committee of the Provincial People's Congress, delivered a speech. To Li Jinbin, Secretary of the Anhui Provincial Party Committee and Director of the Standing Committee of the Provincial People's Congress, delivered a speech. He said that Anhui Province should implement the "national policy" of innovation, creating both a technological peak and a technological plateau. "With Hefei as the core, Wuhu and Bengbu as the two wings, and other cities as the main points, we will speed up the construction of the'five one'. The upgraded version of the main innovation platform and the sub-platforms of'One City, One Center' form a provincial innovation matrix featuring each individual's strengths and benign interaction." Wang Qingxian, Governor of Anhui Province, presided over the opening ceremony of the China (Anhui) Science Fair. To Xu Nanping, Deputy Minister of Science and Technology, delivered a speech. Xu Nanping, Vice Minister of the Ministry of Science and Technology, said in his speech that China (Anhui) Science and Technology Fair will allow more “flowers” of science and technology to produce “fruits” of the industry, and provide solid strategic support for serving and boosting the high-quality development of Anhui and the whole country. Zhang Tao, Vice President of Chinese Academy of Sciences, delivered a speech. In his speech, Zhang Tao, vice president of the Chinese Academy of Sciences, said that at this session of the Science Fair, the Chinese Academy of Sciences will release more than 100 achievement projects, display more than 70 items, and release 5 key projects. "I hope that both parties will take this fair as an opportunity. , Actively docking, and constantly expanding the scope and depth of cooperation. Further focus on the layout and needs of major industries in Anhui Province, actively promote the transformation of high-quality scientific research results of the Chinese Academy of Sciences, form new technologies, create new production capacity, create new business formats, and drive the rapid development of local industries To achieve mutual benefit and win-win results." Li Jinbin, Secretary of the Anhui Provincial Party Committee, kicked the gong for the Anhui Science and Te...
    Read More
  • About the treatment of aluminum alloy products yellowing and blackening (Internet download)
    April 14,2021.

    About the treatment of aluminum alloy products yellowing and blackening (Internet download)

    All the time, the aluminum alloy die casting cleaning is always a difficult problem. The practice of many enterprises is, after machining, do not do thorough cleaning, just use water to simply rinse, then blow dry, or even natural air dry, and then stacked in the warehouse for a few months.Suddenly one day need to be out of the warehouse, only to find the work piece long mildew spot, moldy, black, yellow situation. At this time, we suggest you:  with die-casting aluminum mildew spot cleaning agent timely and thoroughly clean, including the surface of the work piece oil, slight oxidation mildew point (mildew point is still very small, do not look carefully, the naked eye can not really see). after cleaning, immediately do an anti-oxidation treatment. It should be noted that currently chromic acid has been banned, the use of chromium and cyanogen free passivant to meet the environmental requirements. After anti-oxidation drying, the workpiece shall be placed in a dry and ventilated place and inspected regularly. Replacement time Vulnerable workpiece according to the mold production product strain, deformation, fracture, uneven or mold production abnormal sound failure, please replace at any time If it is damaged during assembly or production, please replace the required workpiece at any time. Fragile workpiece Item Replacement time Remark Ejection rod At any time Deformation, fracture, fluff, abnormal sound Cast pin At any time Deformation, fracture Irregularly shaped insert At any time Deformation, fracture Seal ring At any time Leaks, breaks, expiration date Rubber tube At any time Leaks, breaks, expiration date
    Read More
  • About the processing of flying material and adhesive mold on parting surface of mold
    April 14,2021.

    About the processing of flying material and adhesive mold on parting surface of mold

    The mold is composed of moving mold and fixed mold. Parting surface refers to the part that can be contacted when the two are closed.According to the requirements of mold production, the parting surface of the moving and fixed mold core should be 0.15-0.35mm higher than the parting surface of the mold frame (mold frame) to prevent the parting surface from flying materials. 1.It is generally more machine problems that new mold parting surface large area and local parts of the problem of flying material a.Clamping force is small and not locked in place.(empty lock for many times, check the locking strength) b.Is the supercharging pressure too high?Is the trip too short? c.Whether the holding time is too short. d.Is it too warm? (normal position 660° ~ 680°) e.Check die casting machine for wear of curved core (curved arm) or bushing.Is the gap too large? f.Whether the machine wall is balanced 2.The mold will also have problems. a.The mold is not in place. (apply red powder to the smooth and easy to check parting surface of the moving mold core, and (generally apply it to the parting surface of the mold core) after the mold locking, check whether the red powder traces of the parting material surface not applied reach the production requirements of 95% or more. b.Die core exhaust location smaller, shorter or deeper (-0.15mm or more), easy to fly 3.Mass production (more than 25,000 times) of mold parting surface flying material (old mold) a.Check whether the flying material position of parting surface is collapsed, the exhaust groove is too deep or there are foreign matters, such as aluminum slag is not cleaned, so that the mold can not close in place to produce flying material. b.Check whether the height of mold frame (mold frame) and mold core parting surface is in place. The normal closing die is: the upper and lower parting surface of the die core meets each other, and the upper and lower parting surface of the die frame has a gap of 0.3-0.7mm. Long time production products mold deformation, die box around the edge of the upper and lower parting surface hit dead or obviously adhere to foreign bodies, so that the mold core upper and lower parting surface can not touch, can not match to the effective position, resulting in the gap will have flying edge, flying phenomenon.
    Read More
first page 21 22 23 24 25 26 27 28 29 30 last page

A total of 37 pages

leave a message leave a message
If you are interested in our products and want to know more details,please leave a message here,we will reply you as soon as we can.
Home

Products

News

Contact